Shenzhen Wesort Optoelectronics Co., Ltd.
Address:Building 29, Longwangmiao Industrial Zone, Fuyong street, Bao'an District, Shenzhen, Guangdong Province, China.
Phone:+86 181 2370 6862

Coffee is much more than just a beverage—it’s an experience shaped by the quality and consistency of the beans used. Over the years, coffee producers have continually sought ways to improve bean quality, reduce waste, and ensure a uniform flavor profile in every cup. One breakthrough that has dramatically transformed the industry is optical sorting technology. This long-form article explores how modern optical sorting machines are revolutionizing coffee bean processing, drawing insights from industry leaders and cutting-edge manufacturers.
The Evolution of Coffee Bean Sorting
Traditionally, coffee bean sorting was a labor-intensive process that relied on manual inspection. Workers would sort beans by hand, identifying defects, discolorations, and impurities. However, this method was not only time-consuming but also prone to human error and inconsistency. As global demand for high-quality coffee grew, the need for an automated, precise, and efficient sorting solution became undeniable.
Enter optical sorting—a technology that leverages advanced imaging, sensors, and artificial intelligence to identify and remove undesirable beans. According to Counter Culture Coffee, optical sorting represents one of the most exciting advancements in coffee processing, offering a new level of accuracy and efficiency that was previously unattainable in manual sorting processes.

How Optical Sorting Technology Works
At the heart of optical sorting is a sophisticated integration of high-speed cameras, sensors, and intelligent algorithms. Here’s a closer look at the process:
1. High-Resolution Imaging:
Optical sorters use high-resolution cameras to capture detailed images of coffee beans as they pass through the machine at high speeds. This imaging technology is capable of detecting minute differences in color, shape, and size.
2. Sensor Analysis and AI Integration:
Advanced sensors analyze these images in real time. Machine learning algorithms compare the captured images against preset standards for quality. The system is finely tuned to distinguish between healthy beans and those that are discolored, malformed, or otherwise defective. This technology, as highlighted , allows for precise removal of even the smallest impurities, ensuring that only the best beans continue along the production line.
3. Automated Sorting Mechanism:
Once defective beans are identified, the system activates an air jet or mechanical diverter to remove them from the batch. This process is executed in milliseconds, which means the machine can handle large volumes of beans without sacrificing accuracy.

Benefits of Optical Sorting in Coffee Processing
The introduction of optical sorting technology has brought significant improvements across several key areas of coffee production:
- Enhanced Quality and Consistency:
Optical sorters ensure that only beans meeting strict quality standards are used, resulting in a more consistent flavor profile and improved overall quality of the final product. The removal of defective beans not only enhances taste but also prevents undesirable flavors from affecting the brew.
- Increased Efficiency and Reduced Labor Costs:
Automated sorting eliminates the need for labor-intensive manual inspection. This not only speeds up the production process but also reduces labor costs and minimizes human error, leading to a more efficient workflow.
- Minimized Waste and Sustainability Benefits:
By precisely targeting only the defective beans, optical sorters significantly reduce waste. This precise separation contributes to a more sustainable production process by ensuring that a greater proportion of the harvested beans meet the high standards required for premium coffee.
- Improved Traceability and Data Collection:
Modern optical sorters come equipped with data-collection capabilities that allow producers to track the quality of their beans throughout the sorting process. This data can be used to refine production methods, troubleshoot issues, and maintain high-quality standards over time.

Innovations Driving Modern Coffee Sorters
Leading companies in the field have continuously pushed the boundaries of optical sorting technology. For instance, WESORT has developed an advanced colour sorter that utilizes artificial intelligence and state-of-the-art imaging to detect even the subtlest color differences. Their system is designed to adapt and learn from each sorting cycle, improving accuracy and efficiency with every use.
companies like WESORT have integrated these innovations into large-scale production lines, making it possible to process vast quantities of coffee beans without compromising on quality. Their optical sorting solutions are engineered for robustness, speed, and precision—qualities that are indispensable in today’s competitive coffee market.
Industry Impact and Case Studies
The widespread adoption of optical sorting technology is having a transformative effect on the coffee industry. Producers are now able to deliver consistently high-quality products that meet the growing demands of discerning consumers. For example:
- Quality Control:
Coffee roasters and producers report a significant reduction in the number of defective beans reaching the roasting stage. This leads to better tasting coffee and fewer quality-related complaints from customers.
- Operational Efficiency:
The automation provided by optical sorters has streamlined processing operations, enabling companies to scale production without a proportional increase in labor costs. This efficiency has been crucial for meeting rising global demand.
- Market Competitiveness:
By ensuring a consistent and high-quality product, producers using optical sorting technology can position themselves as premium brands in the marketplace. The investment in high-tech sorting solutions often translates into better market prices and stronger brand loyalty.
Future Perspectives
The future of coffee bean processing looks bright, with optical sorting technology set to become even more advanced. Continued advancements in artificial intelligence and sensor technology are expected to further refine sorting accuracy and speed. Integration with Internet of Things (IoT) platforms will enable real-time monitoring and predictive maintenance, ensuring that optical sorting systems are always operating at peak performance.
Moreover, as the coffee industry continues to emphasize sustainability, the precision of optical sorters in reducing waste will become an increasingly important selling point. Future machines may also incorporate more sophisticated data analytics, providing coffee producers with deeper insights into their production processes and opportunities for continuous improvement.
Optical sorting technology represents a significant leap forward in coffee bean processing. By leveraging high-resolution imaging, advanced sensors, and intelligent algorithms, modern optical sorters ensure that only the finest beans make it to your cup. This technology not only enhances product quality and consistency but also drives operational efficiency and sustainability across the coffee supply chain.
Coffee is much more than just a beverage—it’s an experience shaped by the quality and consistency of the beans used. Over the years, coffee producers have continually sought ways to improve bean quality, reduce waste, and ensure a uniform flavor profile in every cup. One breakthrough that has dramatically transformed the industry is optical sorting technology. This long-form article explores how modern optical sorting machines are revolutionizing coffee bean processing, drawing insights from industry leaders and cutting-edge manufacturers.
The Evolution of Coffee Bean Sorting
Traditionally, coffee bean sorting was a labor-intensive process that relied on manual inspection. Workers would sort beans by hand, identifying defects, discolorations, and impurities. However, this method was not only time-consuming but also prone to human error and inconsistency. As global demand for high-quality coffee grew, the need for an automated, precise, and efficient sorting solution became undeniable.
Enter optical sorting—a technology that leverages advanced imaging, sensors, and artificial intelligence to identify and remove undesirable beans. According to Counter Culture Coffee, optical sorting represents one of the most exciting advancements in coffee processing, offering a new level of accuracy and efficiency that was previously unattainable in manual sorting processes.
How Optical Sorting Technology Works
At the heart of optical sorting is a sophisticated integration of high-speed cameras, sensors, and intelligent algorithms. Here’s a closer look at the process:
1. High-Resolution Imaging:
Optical sorters use high-resolution cameras to capture detailed images of coffee beans as they pass through the machine at high speeds. This imaging technology is capable of detecting minute differences in color, shape, and size.
2. Sensor Analysis and AI Integration:
Advanced sensors analyze these images in real time. Machine learning algorithms compare the captured images against preset standards for quality. The system is finely tuned to distinguish between healthy beans and those that are discolored, malformed, or otherwise defective. This technology, as highlighted , allows for precise removal of even the smallest impurities, ensuring that only the best beans continue along the production line.
3. Automated Sorting Mechanism:
Once defective beans are identified, the system activates an air jet or mechanical diverter to remove them from the batch. This process is executed in milliseconds, which means the machine can handle large volumes of beans without sacrificing accuracy.
Benefits of Optical Sorting in Coffee Processing
The introduction of optical sorting technology has brought significant improvements across several key areas of coffee production:
- Enhanced Quality and Consistency:
Optical sorters ensure that only beans meeting strict quality standards are used, resulting in a more consistent flavor profile and improved overall quality of the final product. The removal of defective beans not only enhances taste but also prevents undesirable flavors from affecting the brew.
- Increased Efficiency and Reduced Labor Costs:
Automated sorting eliminates the need for labor-intensive manual inspection. This not only speeds up the production process but also reduces labor costs and minimizes human error, leading to a more efficient workflow.
- Minimized Waste and Sustainability Benefits:
By precisely targeting only the defective beans, optical sorters significantly reduce waste. This precise separation contributes to a more sustainable production process by ensuring that a greater proportion of the harvested beans meet the high standards required for premium coffee.
- Improved Traceability and Data Collection:
Modern optical sorters come equipped with data-collection capabilities that allow producers to track the quality of their beans throughout the sorting process. This data can be used to refine production methods, troubleshoot issues, and maintain high-quality standards over time.
Innovations Driving Modern Coffee Sorters
Leading companies in the field have continuously pushed the boundaries of optical sorting technology. For instance, WESORT has developed an advanced colour sorter that utilizes artificial intelligence and state-of-the-art imaging to detect even the subtlest color differences. Their system is designed to adapt and learn from each sorting cycle, improving accuracy and efficiency with every use.
companies like WESORT have integrated these innovations into large-scale production lines, making it possible to process vast quantities of coffee beans without compromising on quality. Their optical sorting solutions are engineered for robustness, speed, and precision—qualities that are indispensable in today’s competitive coffee market.
Industry Impact and Case Studies
The widespread adoption of optical sorting technology is having a transformative effect on the coffee industry. Producers are now able to deliver consistently high-quality products that meet the growing demands of discerning consumers. For example:
- Quality Control:
Coffee roasters and producers report a significant reduction in the number of defective beans reaching the roasting stage. This leads to better tasting coffee and fewer quality-related complaints from customers.
- Operational Efficiency:
The automation provided by optical sorters has streamlined processing operations, enabling companies to scale production without a proportional increase in labor costs. This efficiency has been crucial for meeting rising global demand.
- Market Competitiveness:
By ensuring a consistent and high-quality product, producers using optical sorting technology can position themselves as premium brands in the marketplace. The investment in high-tech sorting solutions often translates into better market prices and stronger brand loyalty.
Future Perspectives
The future of coffee bean processing looks bright, with optical sorting technology set to become even more advanced. Continued advancements in artificial intelligence and sensor technology are expected to further refine sorting accuracy and speed. Integration with Internet of Things (IoT) platforms will enable real-time monitoring and predictive maintenance, ensuring that optical sorting systems are always operating at peak performance.
Moreover, as the coffee industry continues to emphasize sustainability, the precision of optical sorters in reducing waste will become an increasingly important selling point. Future machines may also incorporate more sophisticated data analytics, providing coffee producers with deeper insights into their production processes and opportunities for continuous improvement.
Optical sorting technology represents a significant leap forward in coffee bean processing. By leveraging high-resolution imaging, advanced sensors, and intelligent algorithms, modern optical sorters ensure that only the finest beans make it to your cup. This technology not only enhances product quality and consistency but also drives operational efficiency and sustainability across the coffee supply chain.
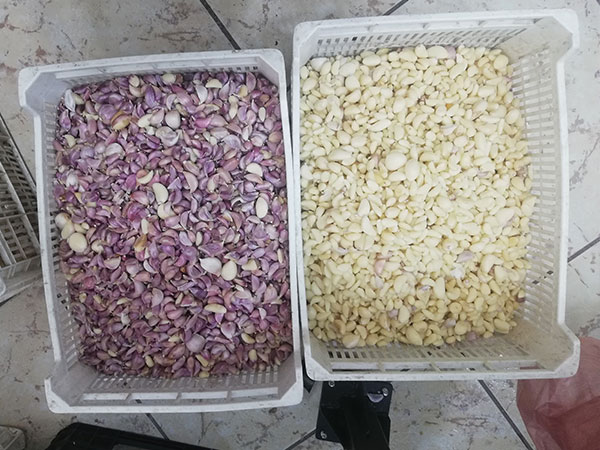
A garlic sorting machine can separate cloves that differ visibly from the accepted product in color, skin coverage, shape, size or surface condition. Typical targets include cloves with attached purple skin, incomplete peeling, yellow or brown disc...
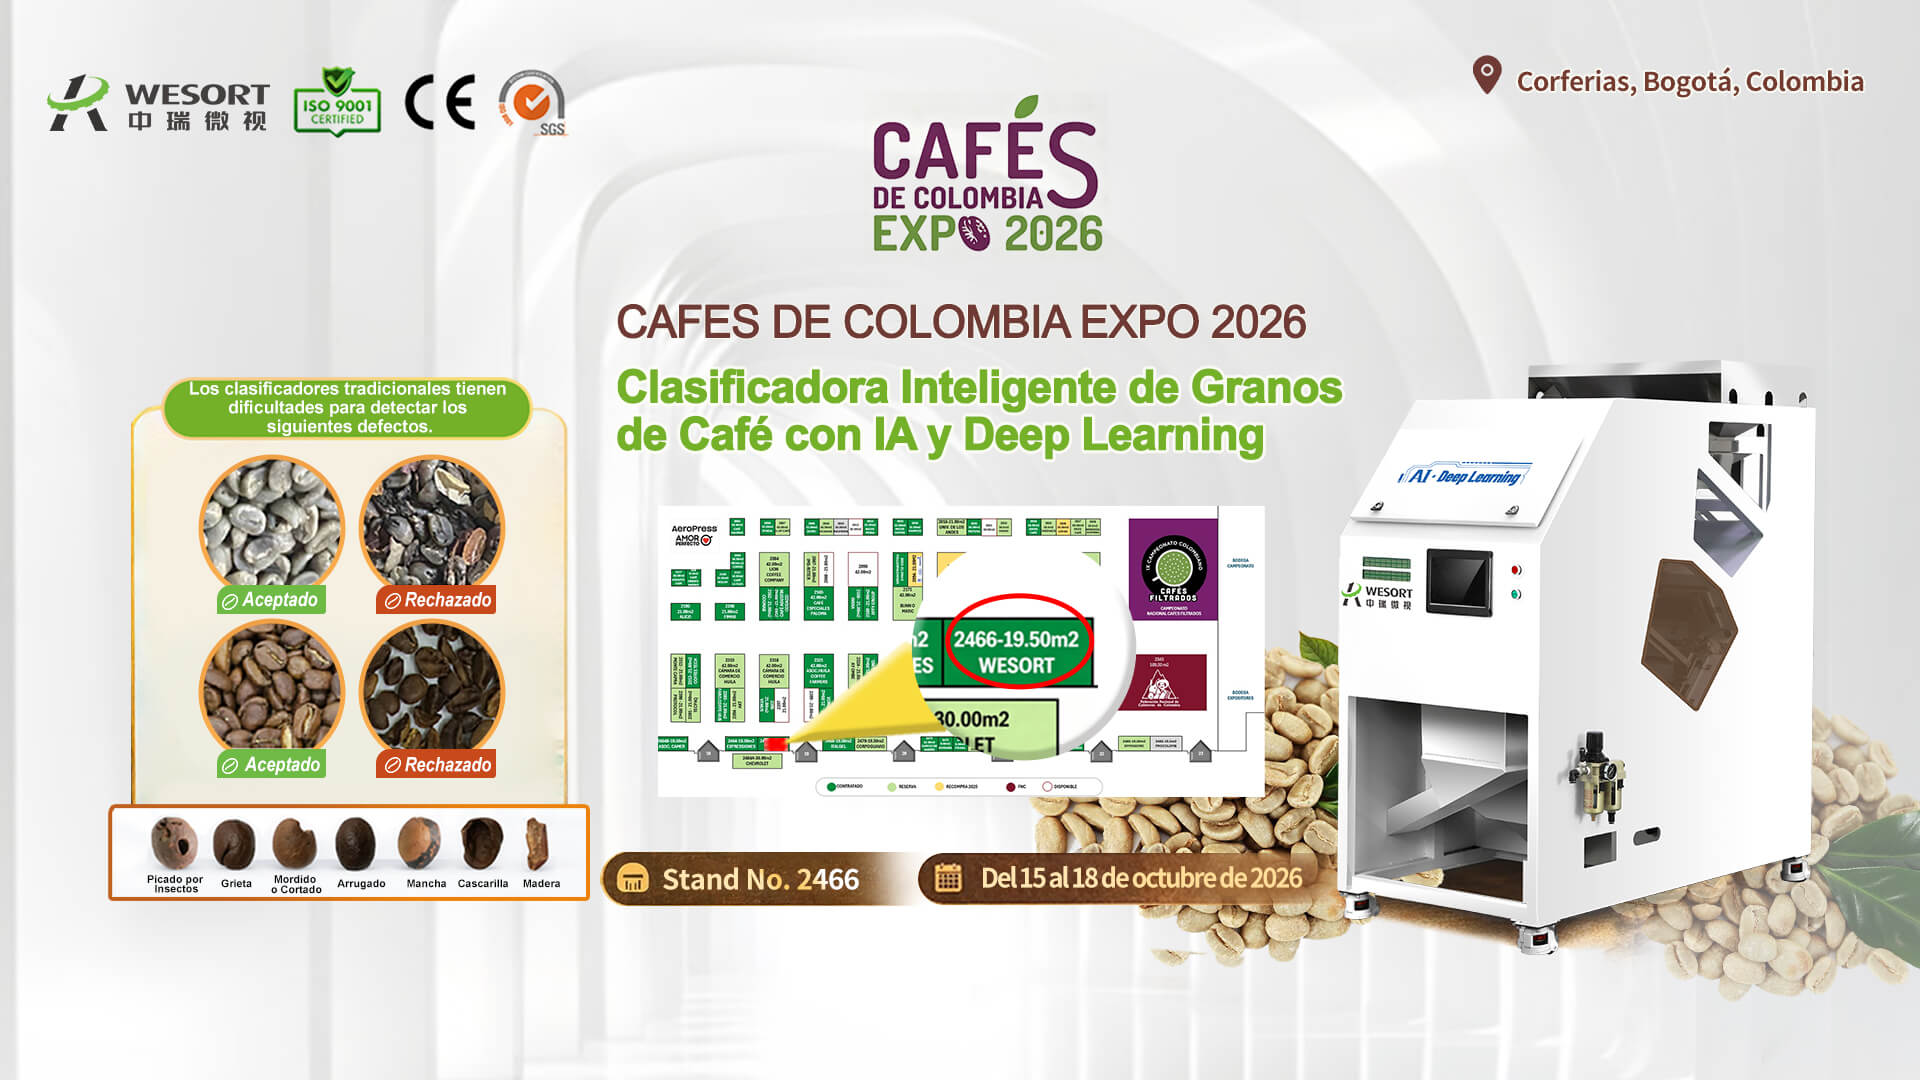
Don’t bring only a business card. Bring the coffee your team is struggling to sort. From October 15 to 18, WESORT will be at Cafés de Colombia Expo 2026 in Bogotá. At Booth 2466, visitors can see how optical sorting responds to real coffee material...
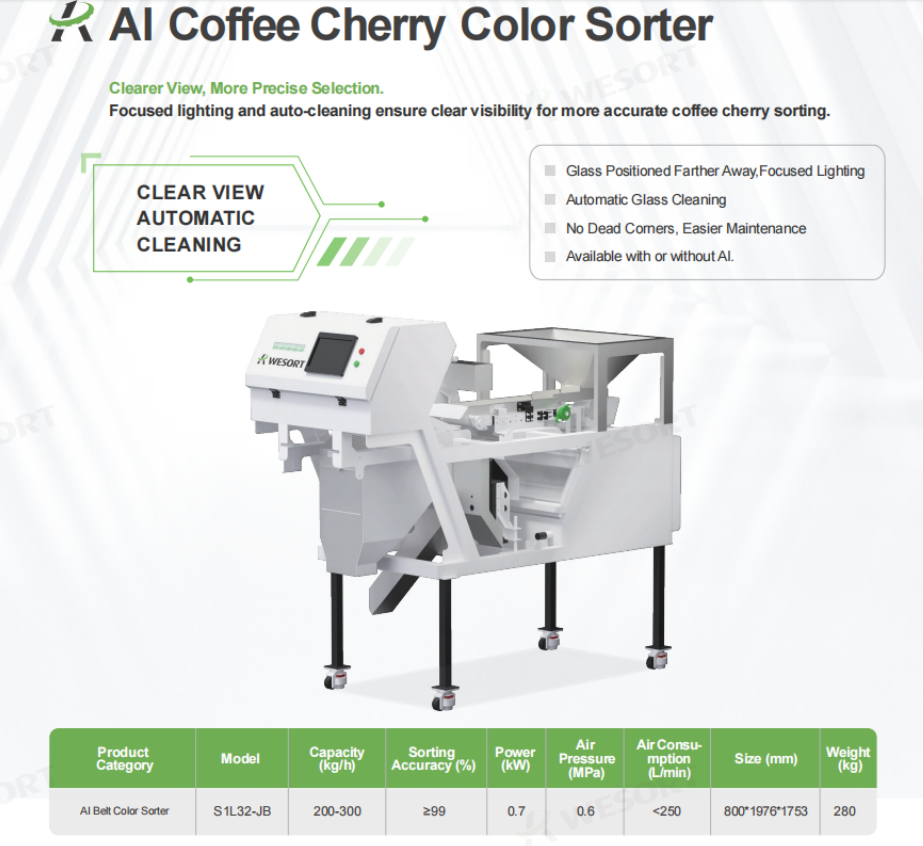
Industry Background and Problem Introduction Coffee processing combines natural variation in agricultural material with increasingly specific buyer and quality requirements. Fresh coffee cherries, parchment coffee, green beans and roasted beans are d...
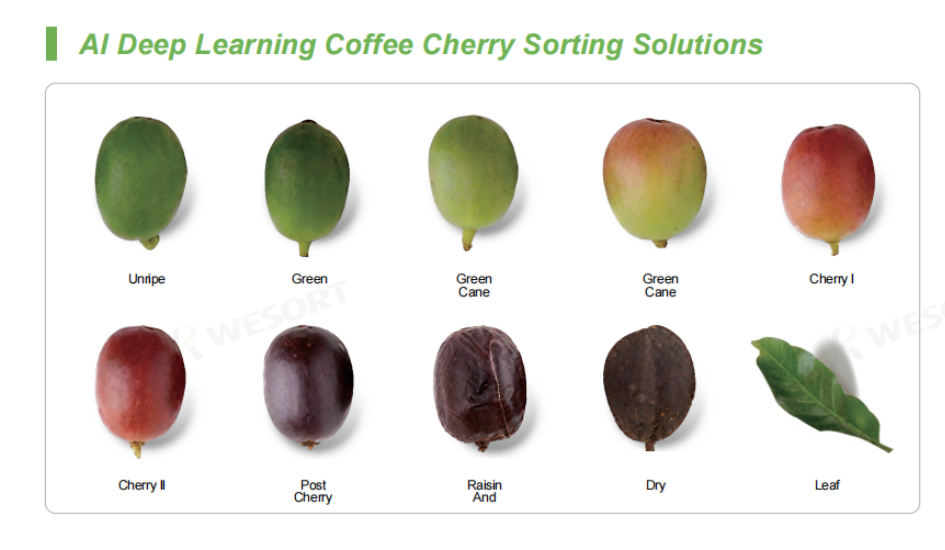
Sorting fresh coffee cherries before pulping or drying can help a processor separate visibly different fruit into more consistent lots. The right approach depends on the cherries, the acceptance standard and where the sorter will sit in the processin...
Table of Contents Start with the bean application Six criteria that affect the real result What WESORT brings to bean sorting How to run a meaningful sample test FAQ The best beans color sorting machine is the one that matches your bean variety, targ...
If you are looking for where to buy a corn color sorter from China, the right starting point is not a marketplace price list. A corn processor needs a manufacturer that can test the actual maize, define the target defects, recommend a suitable machin...
A popular walnut kernel color sorter is not simply the machine with the most attractive specification sheet. Walnut processors need equipment that can recognize black, mold-like, red, yellow, shriveled, broken and shell-containing kernels, maintain s...
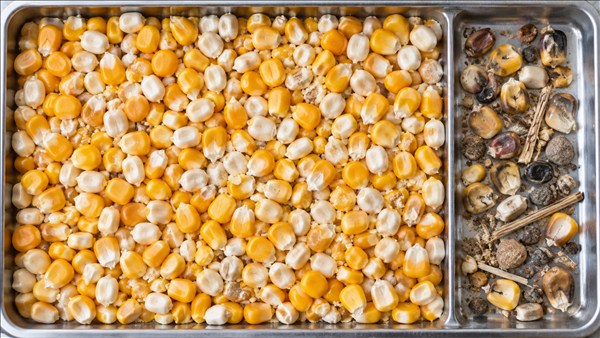
Choosing a corn color sorter for Colombia is not a matter of selecting the lowest price or the largest advertised capacity. The right system must match your corn variety, particle form, visible defects, throughput, utility conditions, downstream proc...
A cracked-walnut line works when every stage has a defined job: clean the mixture, remove shell, separate saleable grades, and control the final packed product. The sorting machine is central to that line, but it performs best when the material reach...
After cracking, walnut processors need to solve two different problems: remove shell efficiently and protect the kernels that carry the selling value. The strongest solution is usually a staged process that combines mechanical separation, infrared sh...
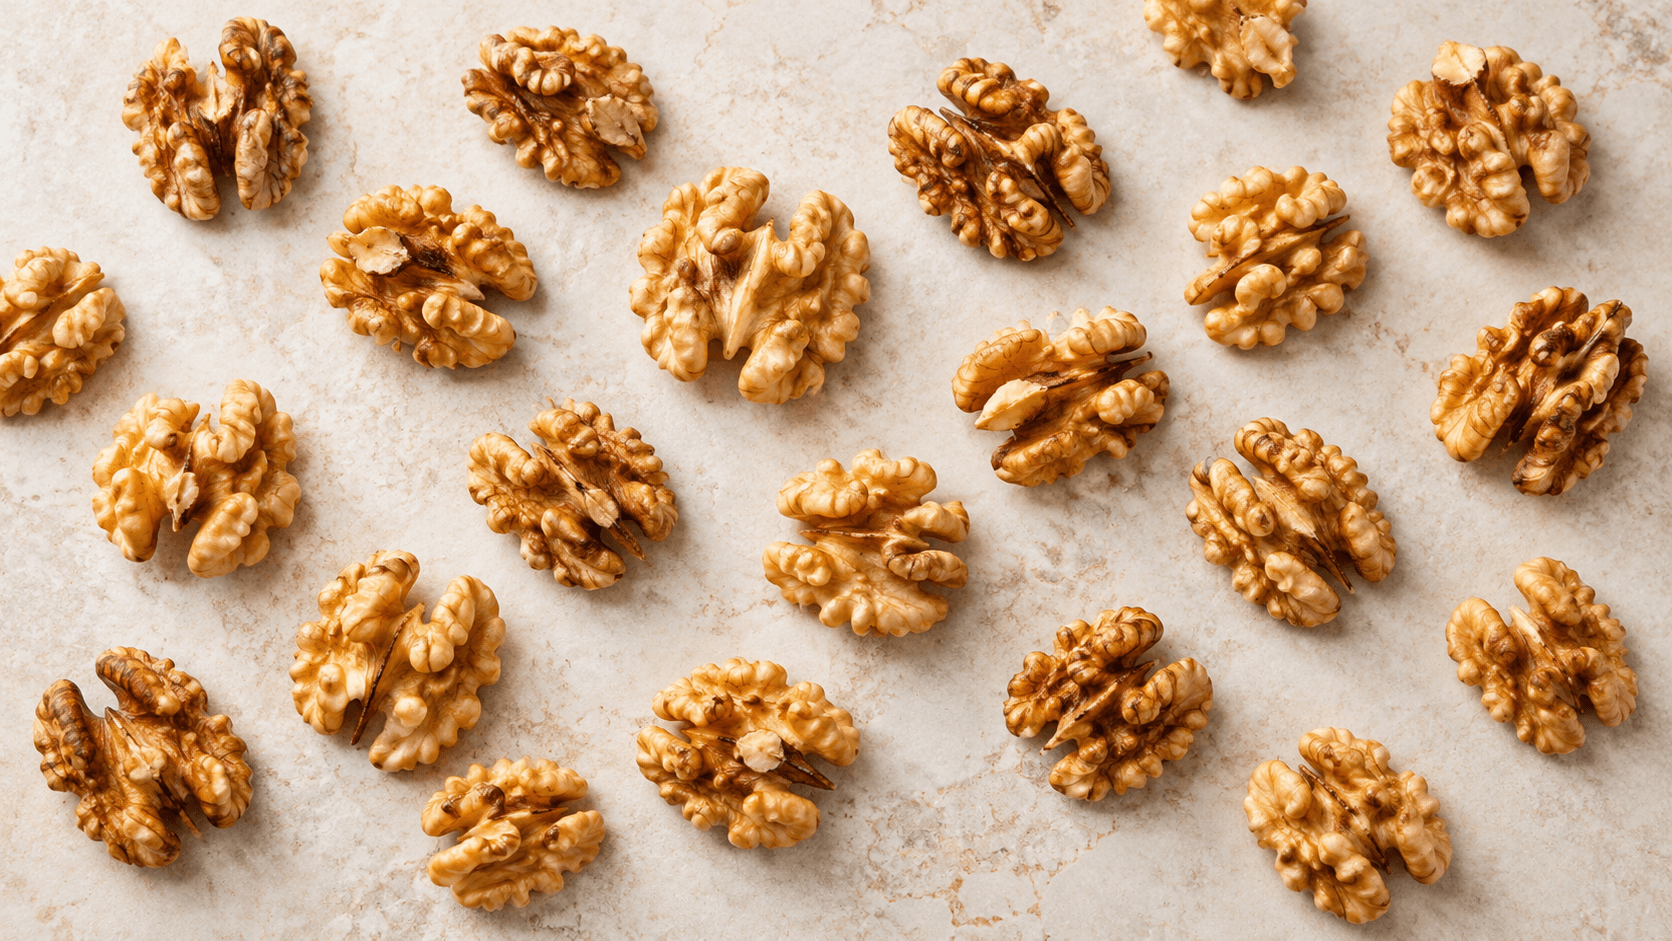
Black, moldy and discolored walnut kernels are not simply “bad colour.” They may represent different grades, different causes and different commercial decisions. WESORT’s AI walnut kernel color sorter converts those visible quality rules into repeata...
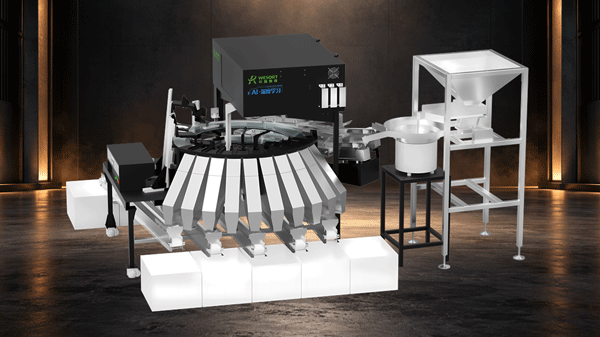
Walnut kernels are commonly sorted with an optical AI sorting machine after cracking, shell separation and preliminary cleaning. The best configuration depends on whether the plant needs colour sorting, visible defect removal, multi-grade separation,...
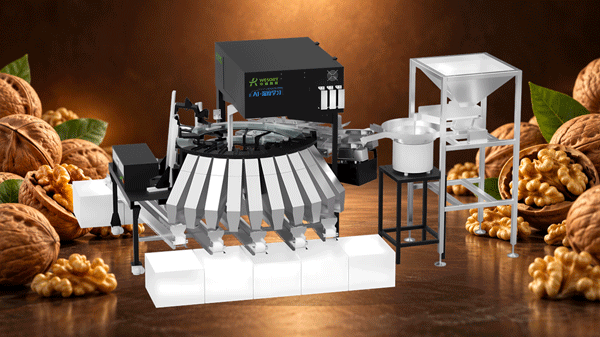
A walnut kernel sorter should do more than remove dark pieces. It should protect valuable halves, separate commercial grades, recognise the visible defects that affect your selling price and fit the way your plant already cracks, cleans, grades and p...
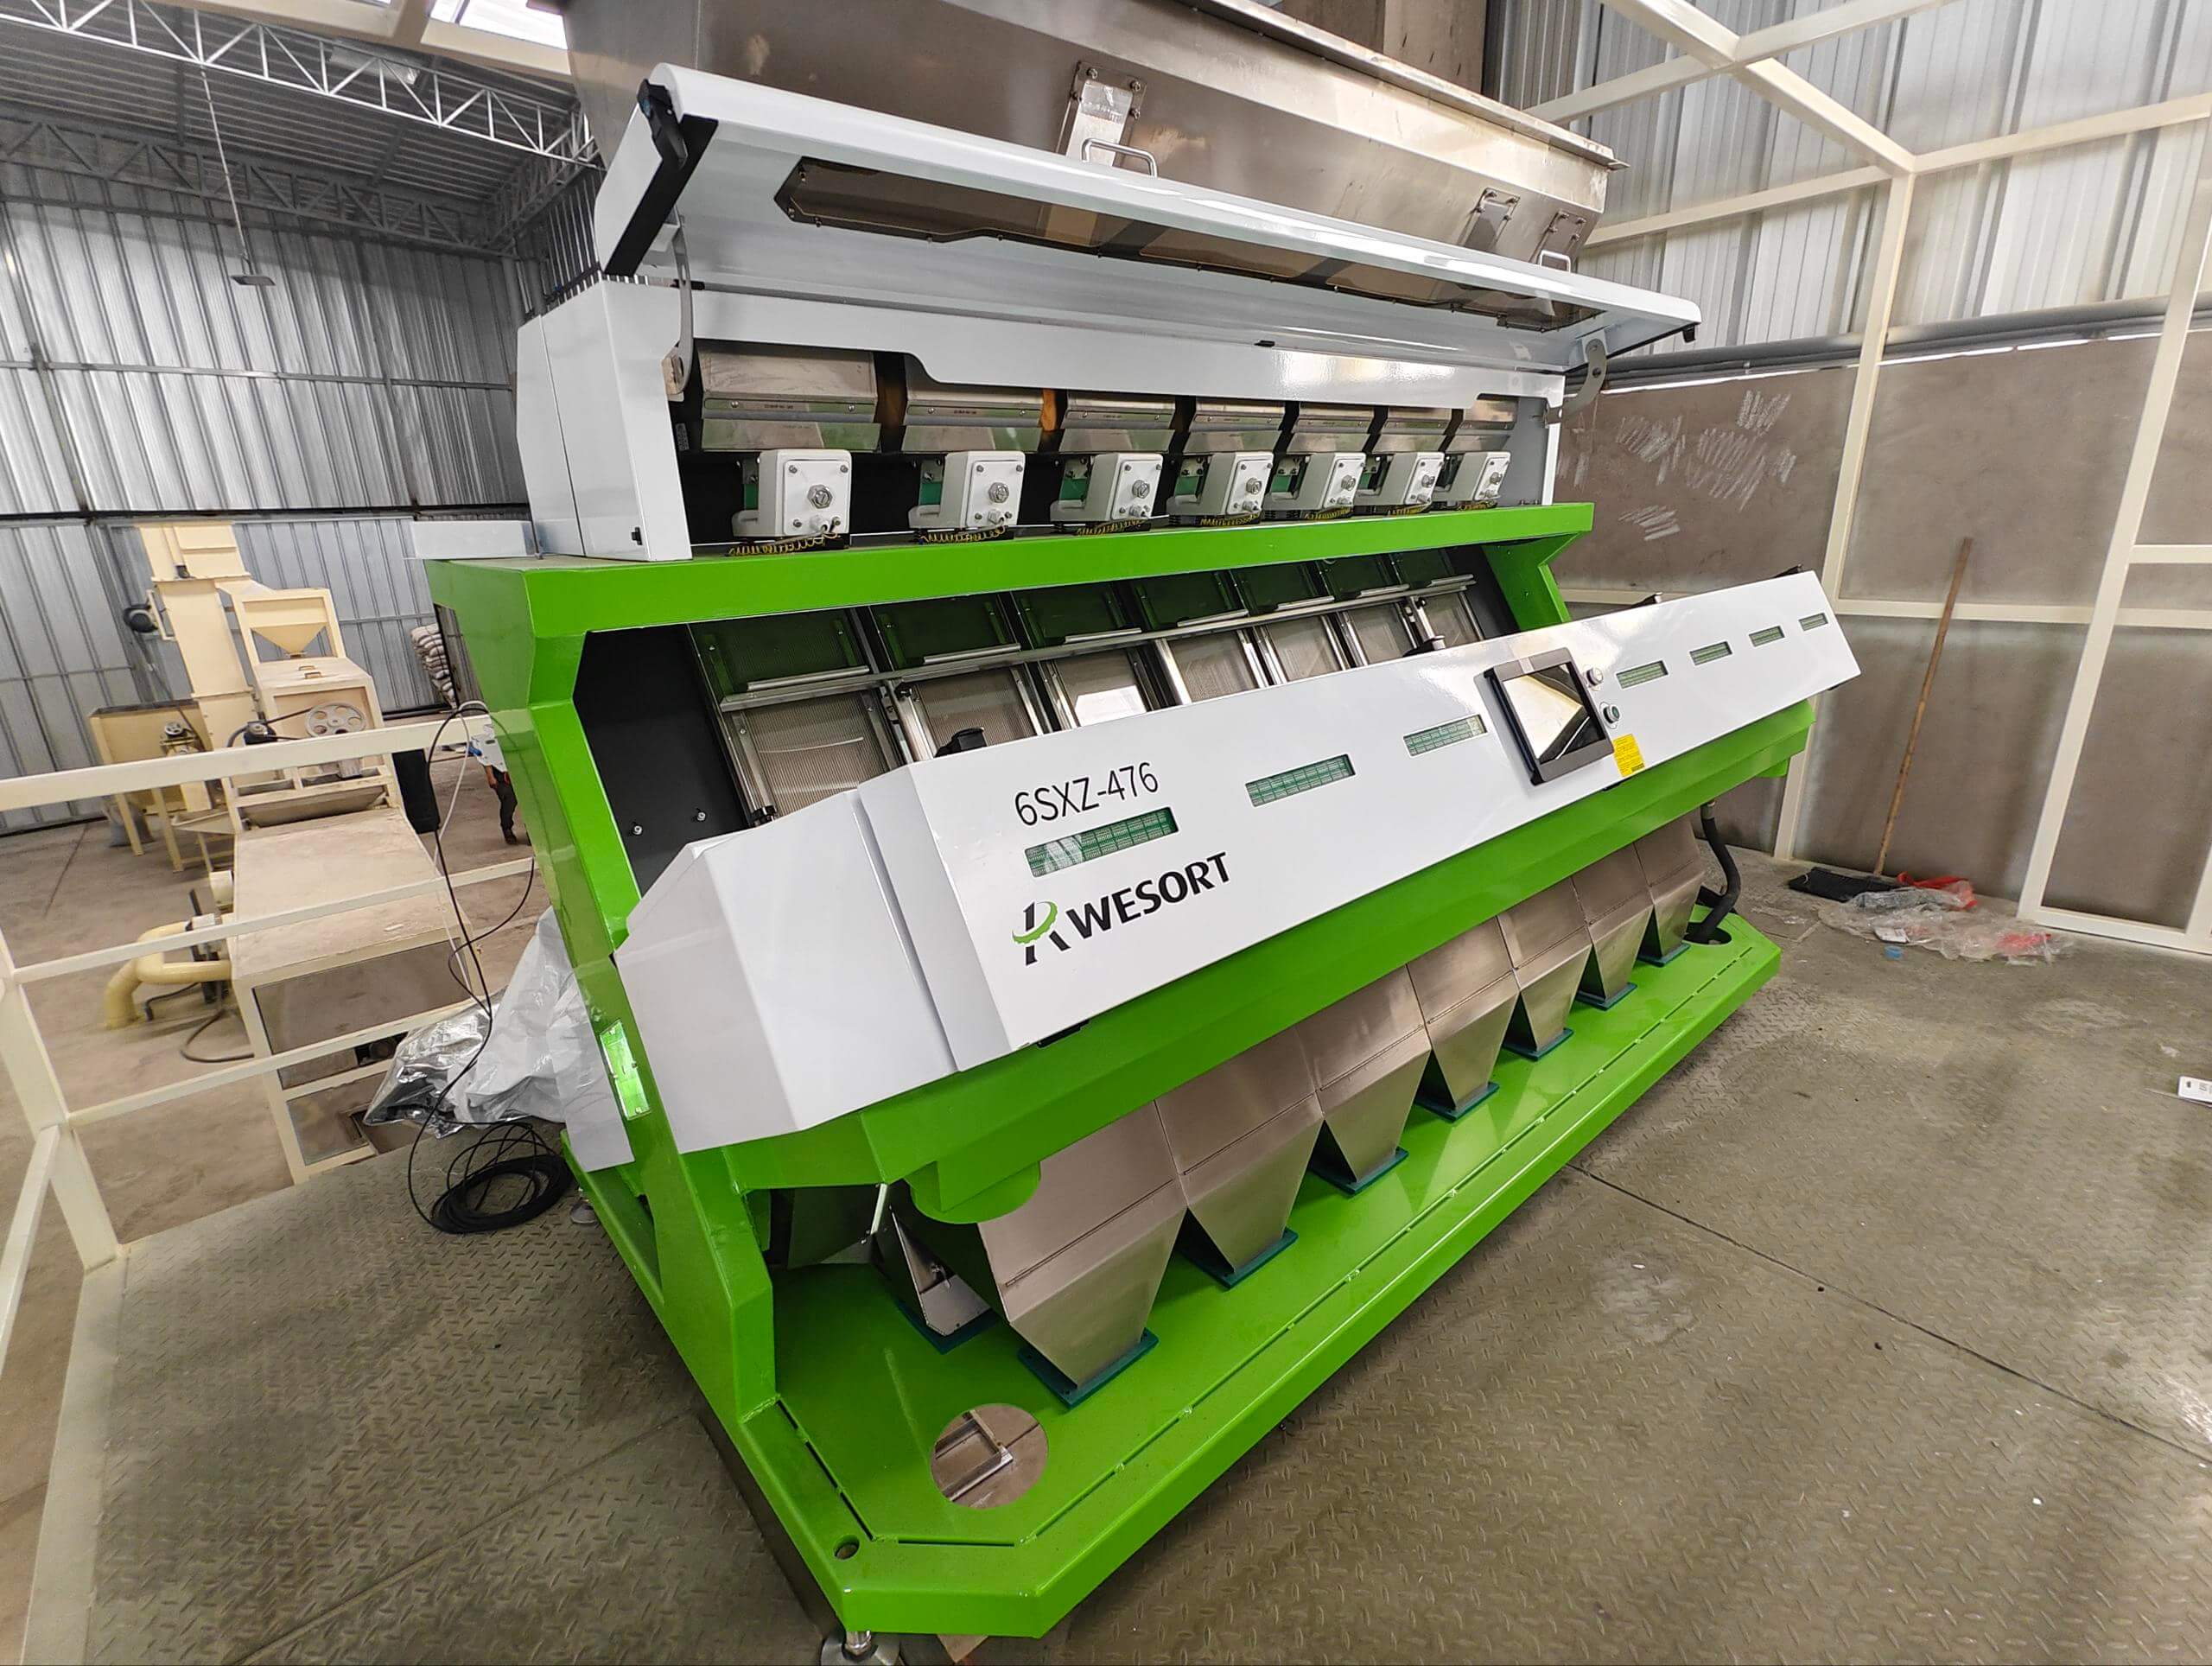
The best bean-sorting result does not begin with a machine setting. It begins with a clear description of the beans you want to pack, the defects your buyer rejects and the amount of good product you are prepared to lose. Short answer: clean and s...
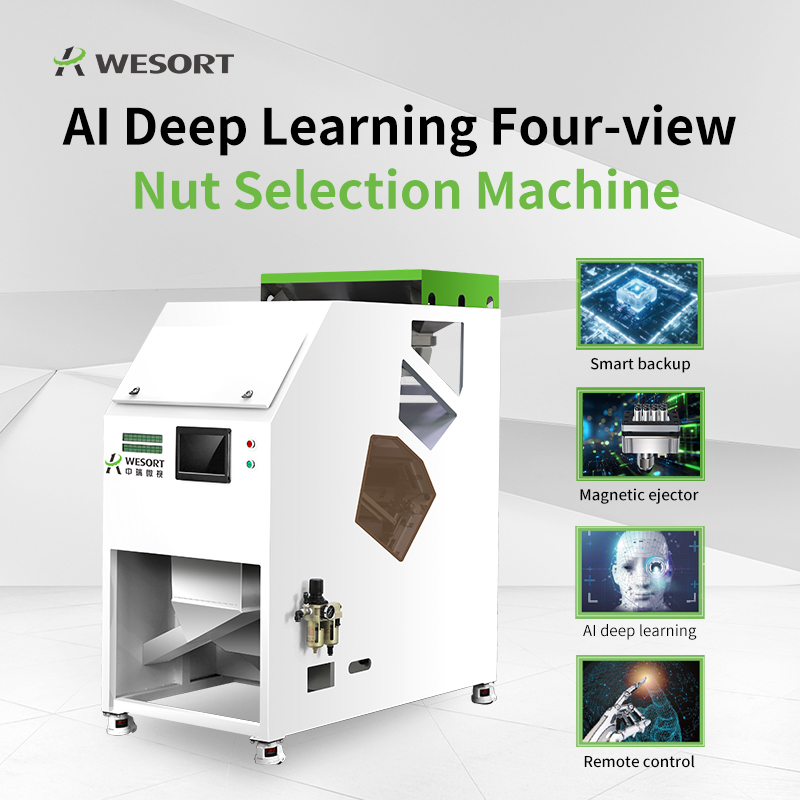
When nut processing enters its busiest weeks, inconsistent raw material, visible defects and foreign materials can quickly become production problems. For processors handling hazelnuts, pistachios, almonds, pecans, Brazil nuts, peanuts and other nut...
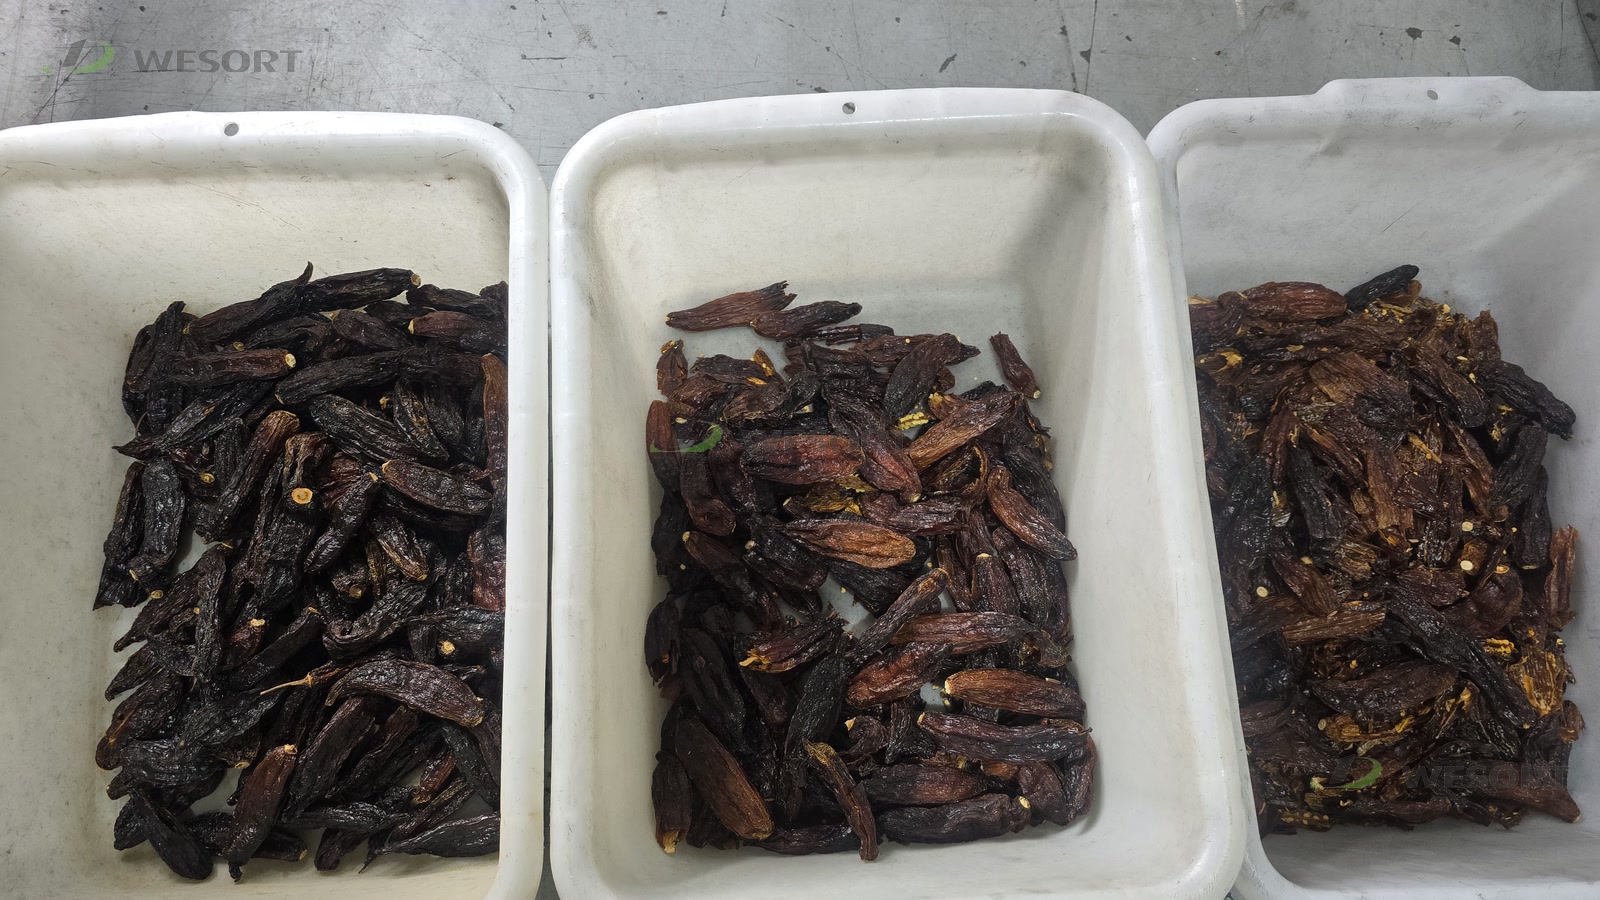
A mixed lot of dried chili rarely has just one problem. Dark pods sit beside red-brown pods, whole product is mixed with broken pieces, and stems or fibrous material remain in the flow. WESORT helps processors turn that mixed lot into clearly defin...
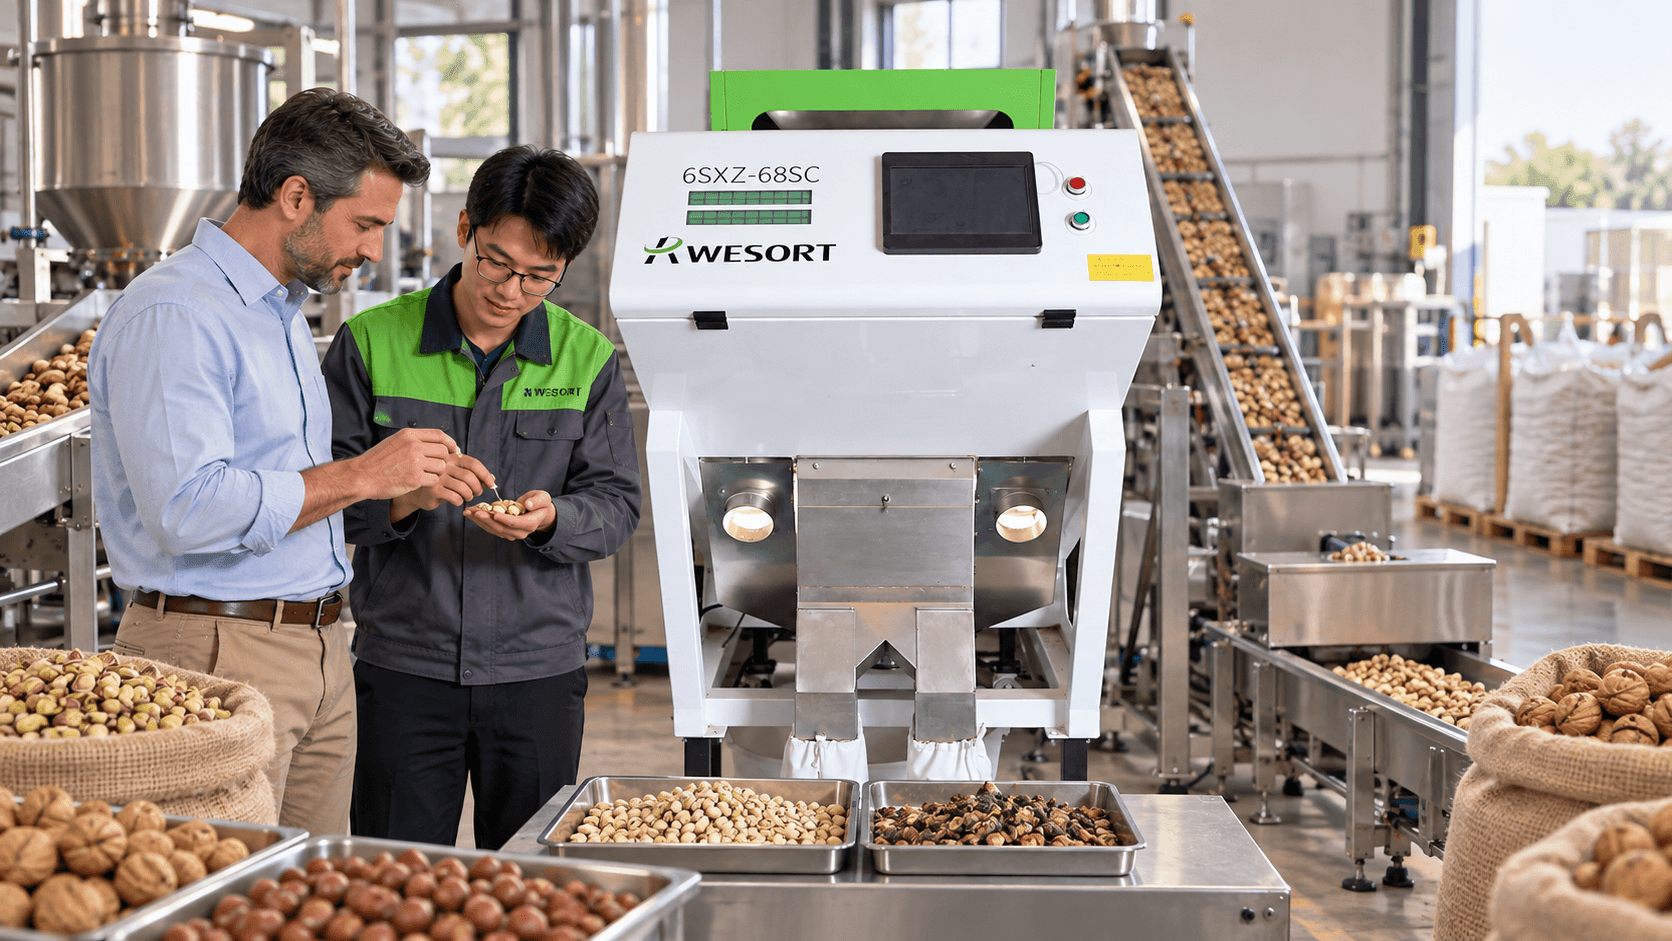
A reliable nut color sorter manufacturer should be able to prove three things before asking you to buy: that your actual material can be separated, that the proposed machine fits your production line, and that technical support will still be availa...
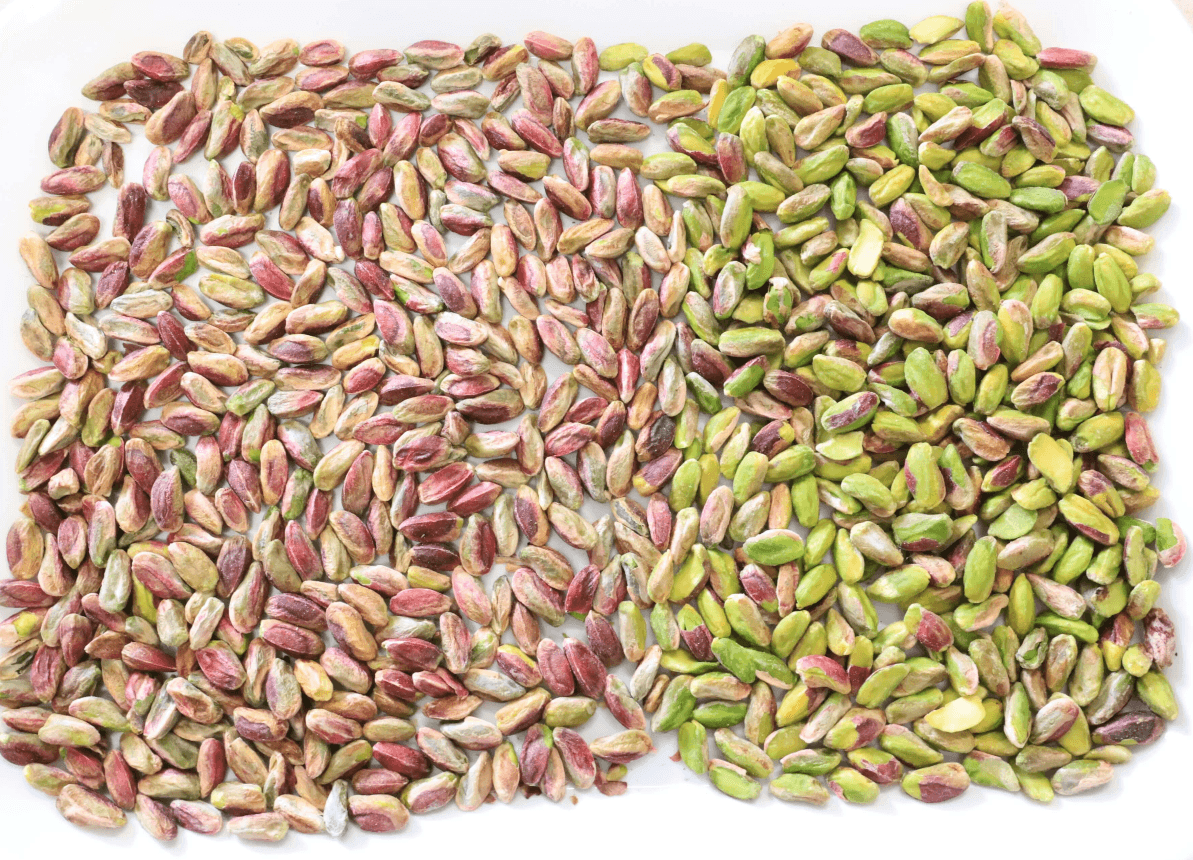
A pistachio sorter should be configured for the material entering it, not for the word “pistachio” alone. An in-shell line may need to separate open and closed shells. A kernel line may need color grades and removal of broken or dark pieces. A post...
Choosing the right pistachio sorting machine in Turkey is not simply a matter of comparing machine width, number of chutes or advertised capacity. For pistachio processors, the more important question is: What exactly does the machine need to sep...
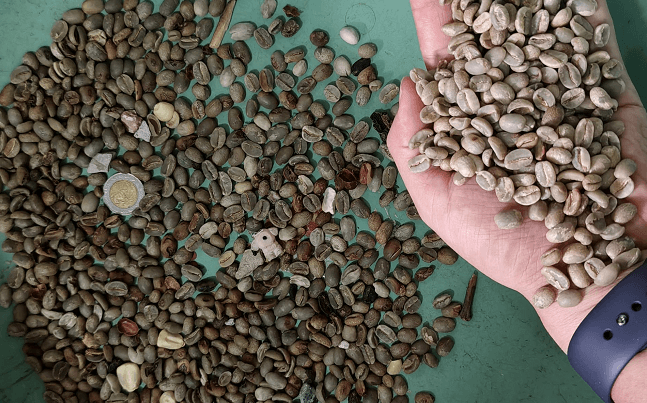
Choosing a coffee sorting machine in Colombia should not begin with the number of chutes or a headline capacity. It should begin with five facts about the coffee entering your line and the product you need to deliver. Without them, two machines th...
A garlic sorting machine can separate cloves that differ visibly from the accepted product in color, skin coverage, shape, size or surface condition. Typical targets include cloves with attached purple skin, incomplete peeling, yellow or brown disc...
Don’t bring only a business card. Bring the coffee your team is struggling to sort. From October 15 to 18, WESORT will be at Cafés de Colombia Expo 2026 in Bogotá. At Booth 2466, visitors can see how optical sorting responds to real coffee material...
Industry Background and Problem Introduction Coffee processing combines natural variation in agricultural material with increasingly specific buyer and quality requirements. Fresh coffee cherries, parchment coffee, green beans and roasted beans are d...
Sorting fresh coffee cherries before pulping or drying can help a processor separate visibly different fruit into more consistent lots. The right approach depends on the cherries, the acceptance standard and where the sorter will sit in the processin...
Table of Contents Start with the bean application Six criteria that affect the real result What WESORT brings to bean sorting How to run a meaningful sample test FAQ The best beans color sorting machine is the one that matches your bean variety, targ...
If you are looking for where to buy a corn color sorter from China, the right starting point is not a marketplace price list. A corn processor needs a manufacturer that can test the actual maize, define the target defects, recommend a suitable machin...
A popular walnut kernel color sorter is not simply the machine with the most attractive specification sheet. Walnut processors need equipment that can recognize black, mold-like, red, yellow, shriveled, broken and shell-containing kernels, maintain s...
Choosing a corn color sorter for Colombia is not a matter of selecting the lowest price or the largest advertised capacity. The right system must match your corn variety, particle form, visible defects, throughput, utility conditions, downstream proc...