Shenzhen Wesort Optoelectronics Co., Ltd.
Address:Building 29, Longwangmiao Industrial Zone, Fuyong street, Bao'an District, Shenzhen, Guangdong Province, China.
Phone:+86 181 2370 6862

If your processing plant is not using a high-quality optical sorter, you may be missing out on an indispensable technology that can improve your production capacity and product quality. Modern Color sorters eliminate the need for time-consuming and inefficient manual sorting. They can handle complex sorting that cannot be accomplished by traditional mechanical sorting, such as air screen cleaners, gravity concentrators, destoners, and creasing machines. These machines can improve your cleaning line's efficiency, accuracy, and quality. A wide range of models is available to match a variety of seed, food, grain, feed, and milling applications and plant capacity.
Many industries, especially agriculture and food processing, have found Color sorters to be an integral part of their operations due to their ability to remove dangerous foreign material such as glass and stone. These machines can quickly sort many different types of materials.
Color sorters, also known as Color sorters have had a transformative impact on seed and grain processing plants. They can identify the characteristics of the raw materials passing through the machine and sort them based on color, size, quality, and kernel defects. Rejected grains are ejected from the acceptable product along with other grains, foreign material such as stones and glass. Defective material is any material that contains impurities such as discolored fragments, foreign matter, damaged seeds, or diseased kernels. Using an optical sorter to remove these foreign materials can extend the life of downstream equipment while ensuring the safety of the finished product.
Most Color sorters use several types of high-definition cameras to view the kernels in the visible spectrum, just as the human eye does, but also to view the kernels at wavelengths outside the range that the human eye cannot see, allowing for more difficult separations. For example, dark grains and dark kernels appear the same color to the human eye, but cameras outside the wavelength range that the human eye cannot see can distinguish them and remove the kernels. The cameras in an optical sorter can be programmed to use a variety of sorting criteria: color, size, shape, texture, disease, and pests are some common examples. The imaging technology is so precise that the cameras can be fine-tuned to the exact color of the product and quickly reject mismatched products, which is very useful when consumers expect uniform products.

Years ago, before automated machines became widely available, all sorting was done manually. As you can imagine, this manual process was extremely time-consuming, inefficient, and inaccurate. Mechanical grain sorters were the next evolution in efficiency and quality in grain handling plants, and are still manufactured and used today in plants around the world. These mechanical sorters include air screen cleaners, toothed drum sorters, gravity concentrators, and destoners, to name a few. Modern plants are improving the quality and efficiency of mechanical sorting by adding color sorters as a new step in existing processes, or replacing them entirely in certain grains, to improve product quality and reduce operating costs. Color sorting technology can catch defects that the human eye can’t see, ensuring that product quality is consistent day after day and shift after shift, and adding a sorting tool with visual effects that mechanical sorters can’t achieve.
Like any machine, color sorters need to be properly maintained to keep them performing at their best. Even the best color sorters can suffer from performance degradation if they are not cleaned or maintained. Regular maintenance is essential to protecting your investment and ensuring your operation runs smoothly.
It is critical to keep all parts of your color sorter clean and mechanically maintained. Dust filters need to be checked and cleaned regularly. Another way to extend the life of your machine is to monitor the air quality of the compressor. If you find that the compressed air contains moisture, oil, or dust, it may mean that the internal valve mechanism is faulty and needs to be replaced.
Once you have confirmed that the machine is clean and running well, check the performance of the software and sensors. While this basic monitoring is becoming increasingly automated, operators still need to keep a close eye on real-time conditions. For example, older color sorters may still require manual calibration, but newer generation color sorters eliminate this need through the use of internal calibration algorithms. Like any computer system, the color sorter's database and parameter settings need to be backed up regularly.
Of course, the best way to maintain your color sorter is to hire a professional like WESORT. Our experienced and certified technicians can perform regular preventive maintenance to help you protect your valuable equipment and avoid unexpected downtime.
Integrating a color sorter into your processing flow can save you time and money while improving your overall output and quality. To learn more about improving operational efficiency, check out our blog!
If your processing plant is not using a high-quality optical sorter, you may be missing out on an indispensable technology that can improve your production capacity and product quality. Modern Color sorters eliminate the need for time-consuming and inefficient manual sorting. They can handle complex sorting that cannot be accomplished by traditional mechanical sorting, such as air screen cleaners, gravity concentrators, destoners, and creasing machines. These machines can improve your cleaning line's efficiency, accuracy, and quality. A wide range of models is available to match a variety of seed, food, grain, feed, and milling applications and plant capacity.
Many industries, especially agriculture and food processing, have found Color sorters to be an integral part of their operations due to their ability to remove dangerous foreign material such as glass and stone. These machines can quickly sort many different types of materials.
Color sorters, also known as Color sorters have had a transformative impact on seed and grain processing plants. They can identify the characteristics of the raw materials passing through the machine and sort them based on color, size, quality, and kernel defects. Rejected grains are ejected from the acceptable product along with other grains, foreign material such as stones and glass. Defective material is any material that contains impurities such as discolored fragments, foreign matter, damaged seeds, or diseased kernels. Using an optical sorter to remove these foreign materials can extend the life of downstream equipment while ensuring the safety of the finished product.
Most Color sorters use several types of high-definition cameras to view the kernels in the visible spectrum, just as the human eye does, but also to view the kernels at wavelengths outside the range that the human eye cannot see, allowing for more difficult separations. For example, dark grains and dark kernels appear the same color to the human eye, but cameras outside the wavelength range that the human eye cannot see can distinguish them and remove the kernels. The cameras in an optical sorter can be programmed to use a variety of sorting criteria: color, size, shape, texture, disease, and pests are some common examples. The imaging technology is so precise that the cameras can be fine-tuned to the exact color of the product and quickly reject mismatched products, which is very useful when consumers expect uniform products.
Years ago, before automated machines became widely available, all sorting was done manually. As you can imagine, this manual process was extremely time-consuming, inefficient, and inaccurate. Mechanical grain sorters were the next evolution in efficiency and quality in grain handling plants, and are still manufactured and used today in plants around the world. These mechanical sorters include air screen cleaners, toothed drum sorters, gravity concentrators, and destoners, to name a few. Modern plants are improving the quality and efficiency of mechanical sorting by adding color sorters as a new step in existing processes, or replacing them entirely in certain grains, to improve product quality and reduce operating costs. Color sorting technology can catch defects that the human eye can’t see, ensuring that product quality is consistent day after day and shift after shift, and adding a sorting tool with visual effects that mechanical sorters can’t achieve.
Like any machine, color sorters need to be properly maintained to keep them performing at their best. Even the best color sorters can suffer from performance degradation if they are not cleaned or maintained. Regular maintenance is essential to protecting your investment and ensuring your operation runs smoothly.
It is critical to keep all parts of your color sorter clean and mechanically maintained. Dust filters need to be checked and cleaned regularly. Another way to extend the life of your machine is to monitor the air quality of the compressor. If you find that the compressed air contains moisture, oil, or dust, it may mean that the internal valve mechanism is faulty and needs to be replaced.
Once you have confirmed that the machine is clean and running well, check the performance of the software and sensors. While this basic monitoring is becoming increasingly automated, operators still need to keep a close eye on real-time conditions. For example, older color sorters may still require manual calibration, but newer generation color sorters eliminate this need through the use of internal calibration algorithms. Like any computer system, the color sorter's database and parameter settings need to be backed up regularly.
Of course, the best way to maintain your color sorter is to hire a professional like WESORT. Our experienced and certified technicians can perform regular preventive maintenance to help you protect your valuable equipment and avoid unexpected downtime.
Integrating a color sorter into your processing flow can save you time and money while improving your overall output and quality. To learn more about improving operational efficiency, check out our blog!
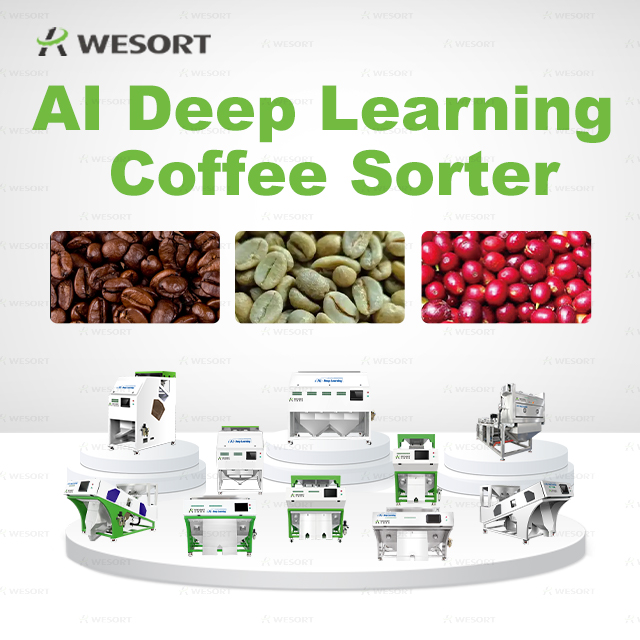
Mexico has a strong coffee-processing industry, with coffee producers and processors facing increasingly demanding requirements for quality, consistency, and production efficiency. From coffee cherries and green coffee beans to roasted coffee, effect...
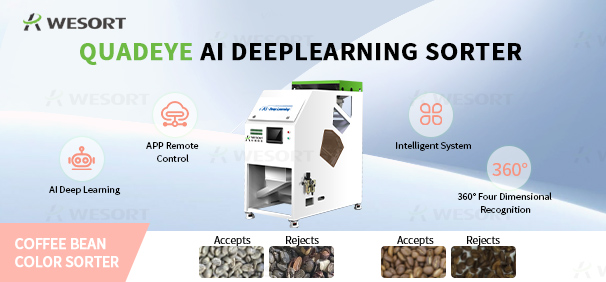
Coffee quality control depends heavily on the equipment used to remove defective beans, foreign materials, and quality inconsistencies before roasting or export. For coffee processors, roasteries, and exporters, AI-powered optical color sorters h...
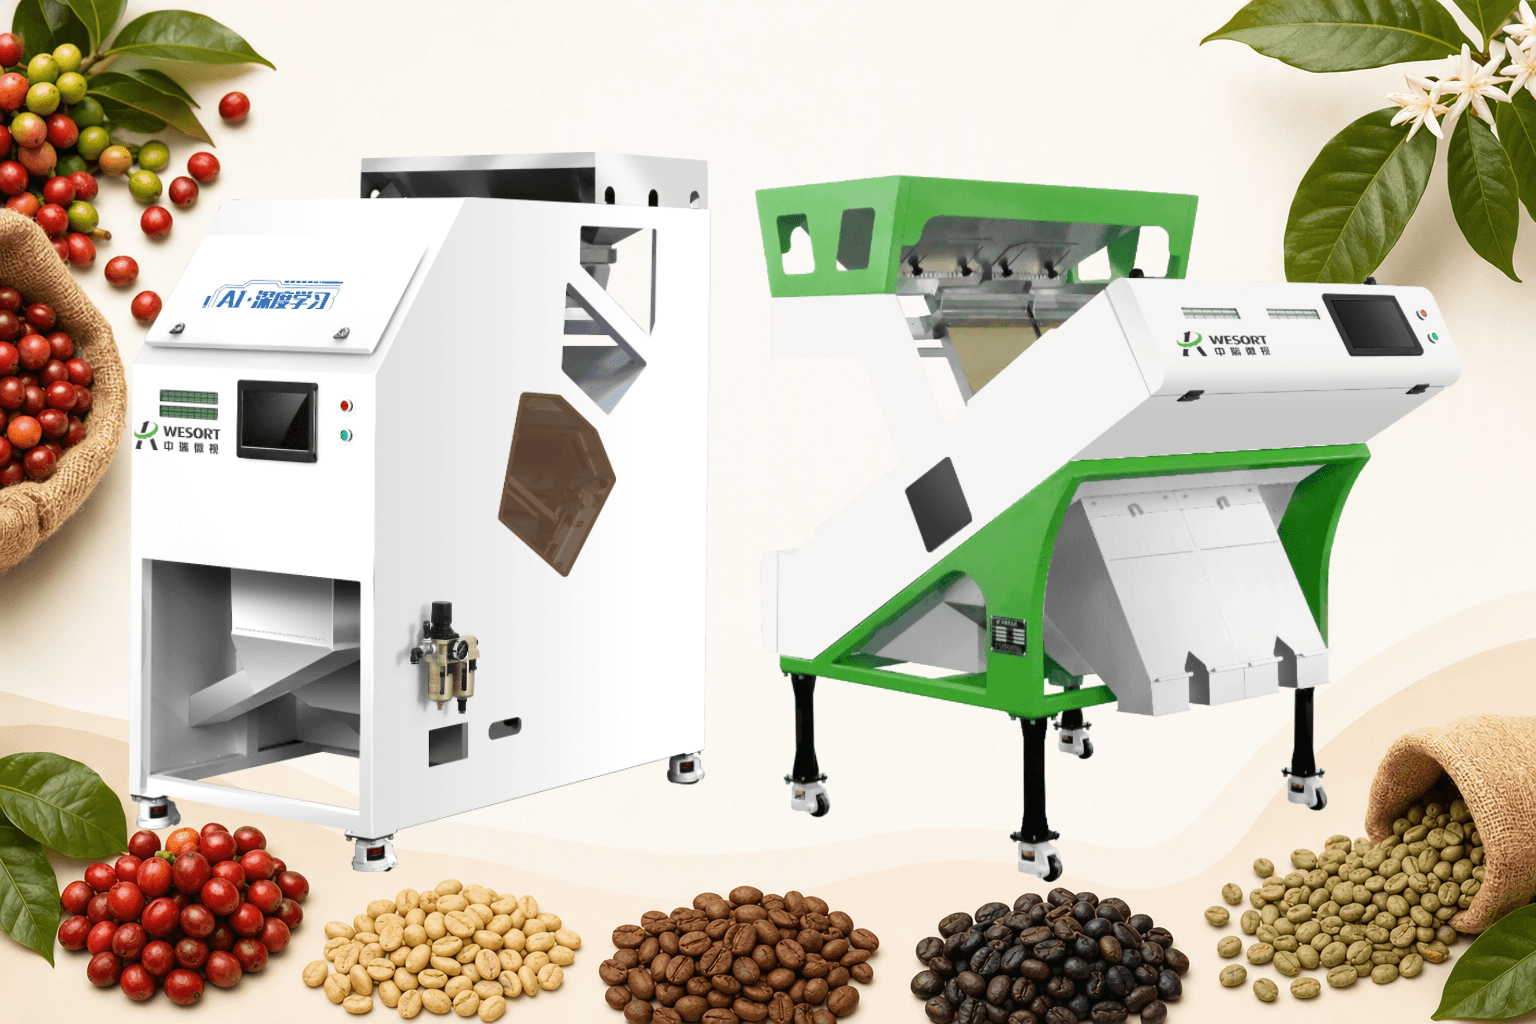
Coffee processors around the world are under growing pressure to deliver consistent quality while controlling costs and meeting strict export standards. Manual sorting—long the default method for removing quakers, scorched beans, and foreign matter...
Upgrade Your Sorting Solution with Exclusive Benefits In 2026. WESORT continues to move forward with innovation, quality, and commitment. We sincerely appreciate the trust and support from customers around the world. To give back to our global ...
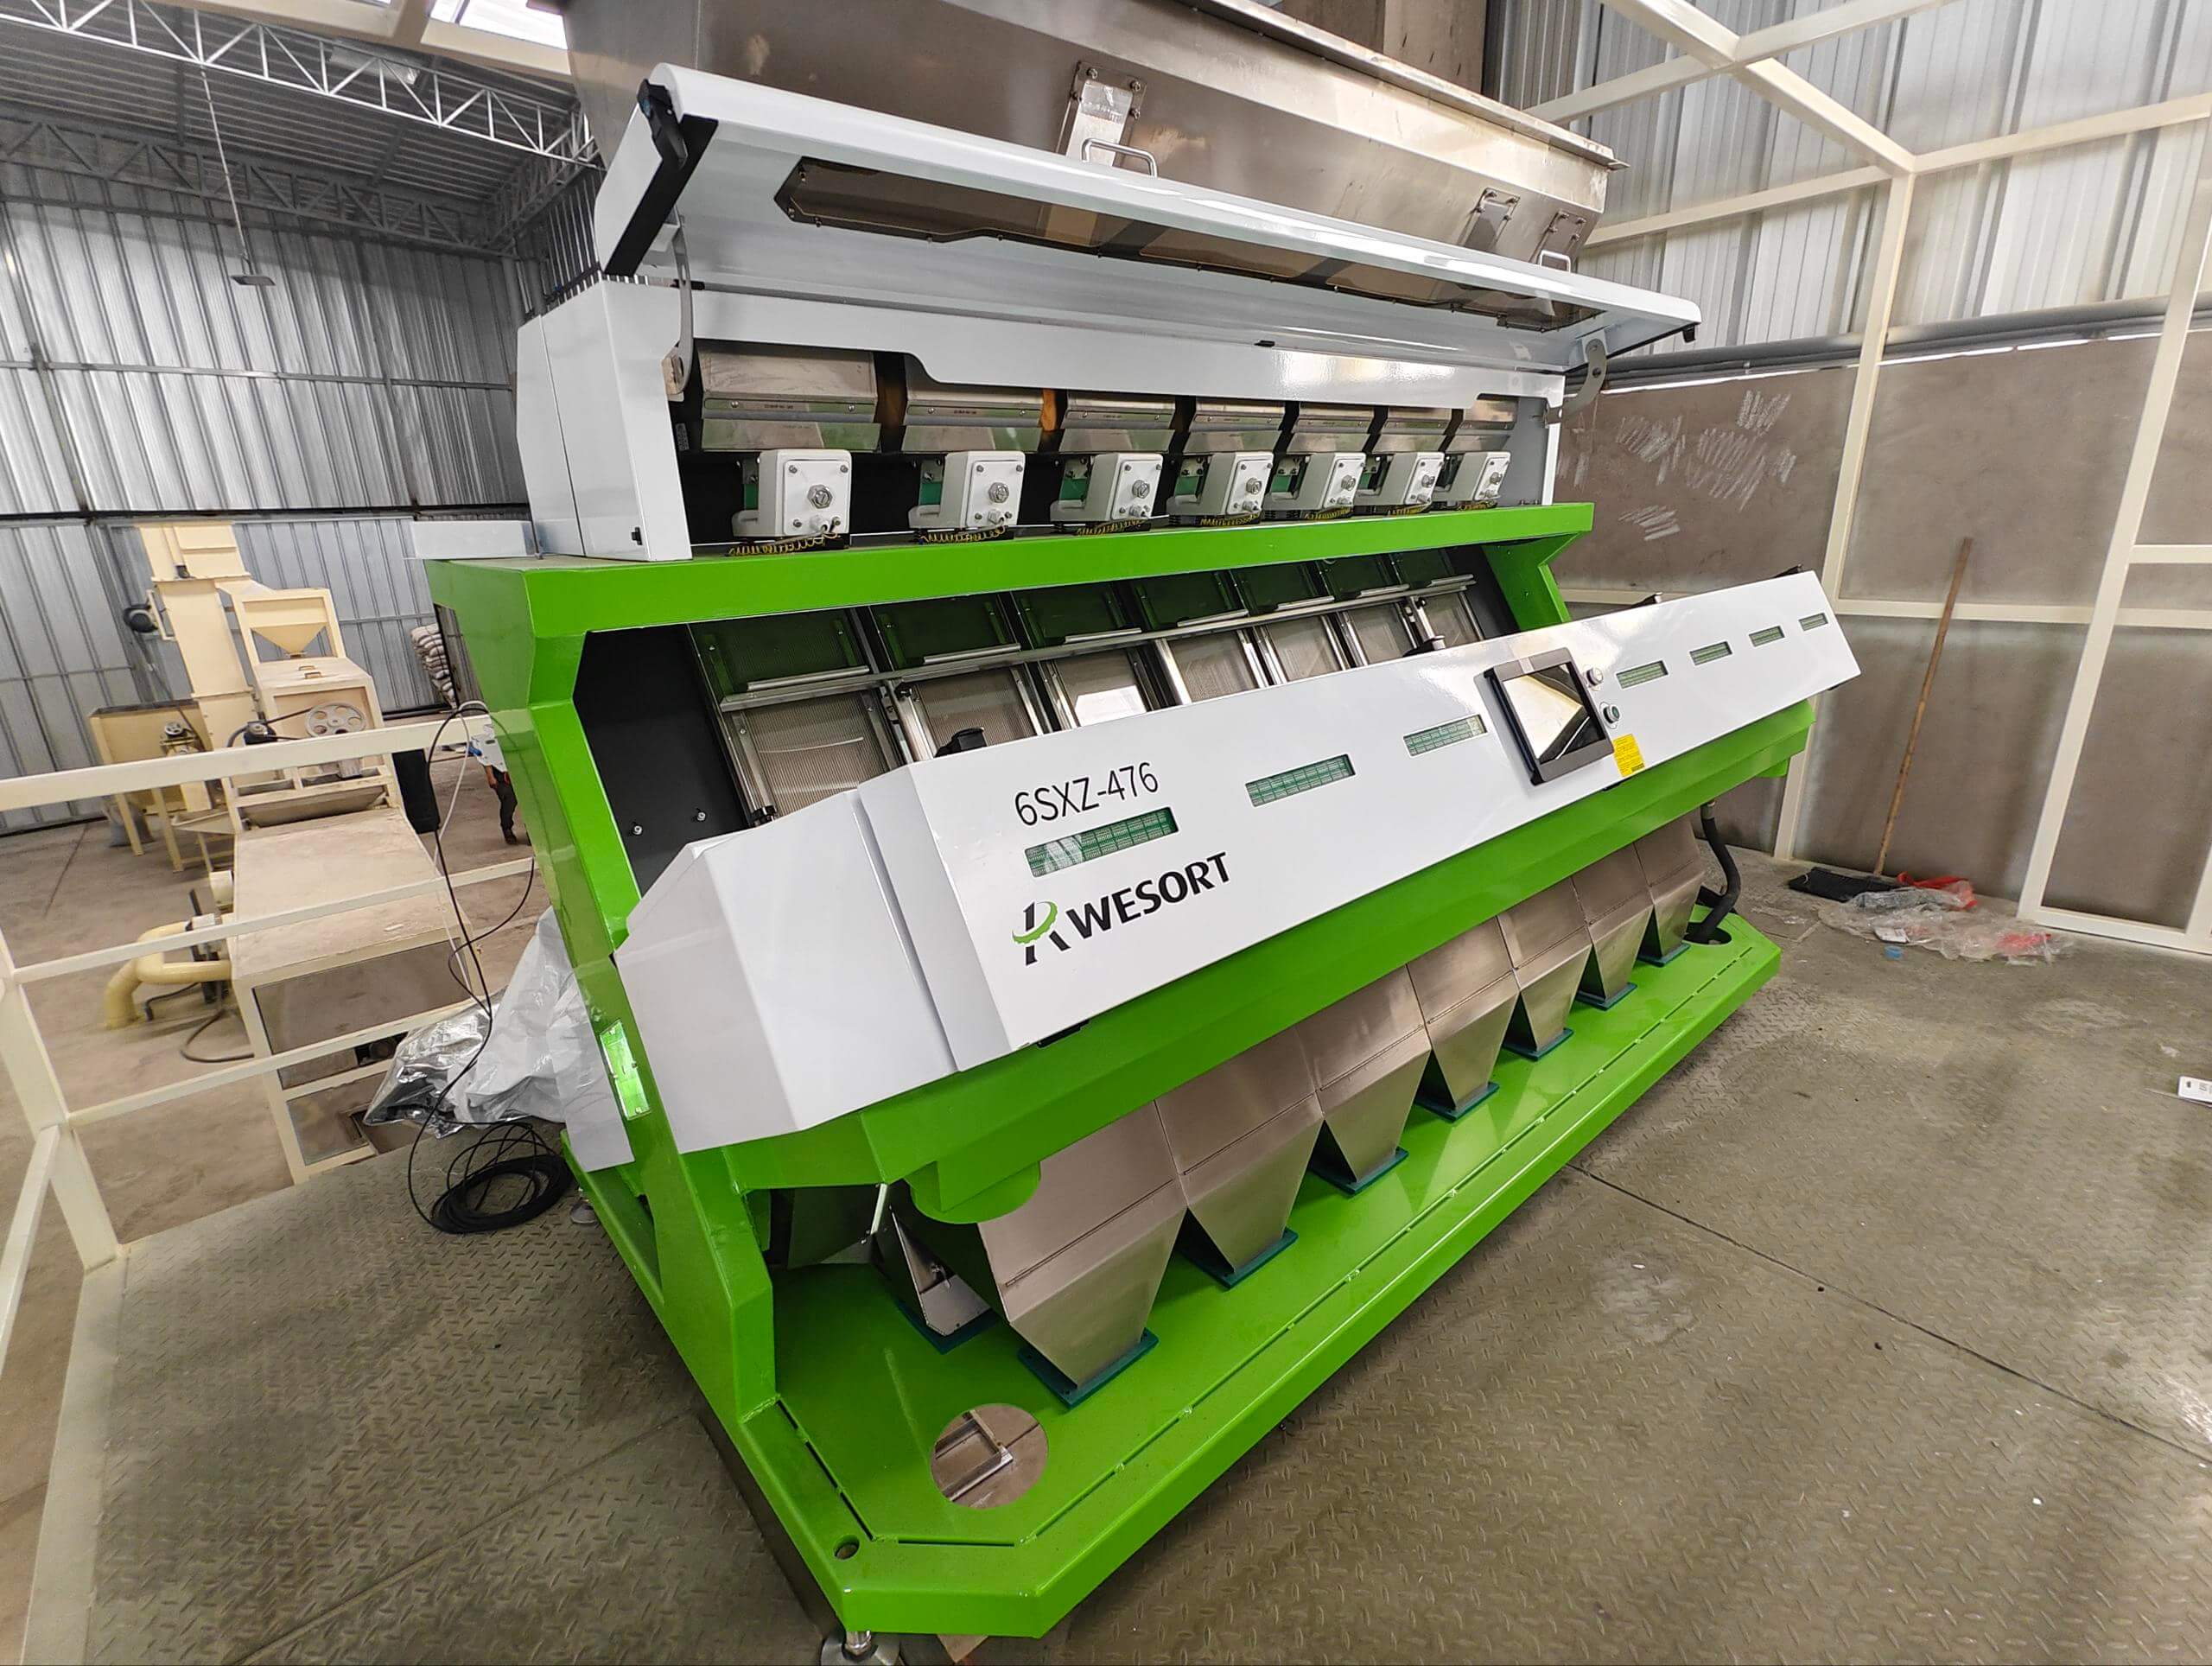
The best bean-sorting result does not begin with a machine setting. It begins with a clear description of the beans you want to pack, the defects your buyer rejects and the amount of good product you are prepared to lose. Short answer: clean and s...
When nut processing enters its busiest weeks, inconsistent raw material, visible defects and foreign materials can quickly become production problems. For processors handling hazelnuts, pistachios, almonds, pecans, Brazil nuts, peanuts and other nut...
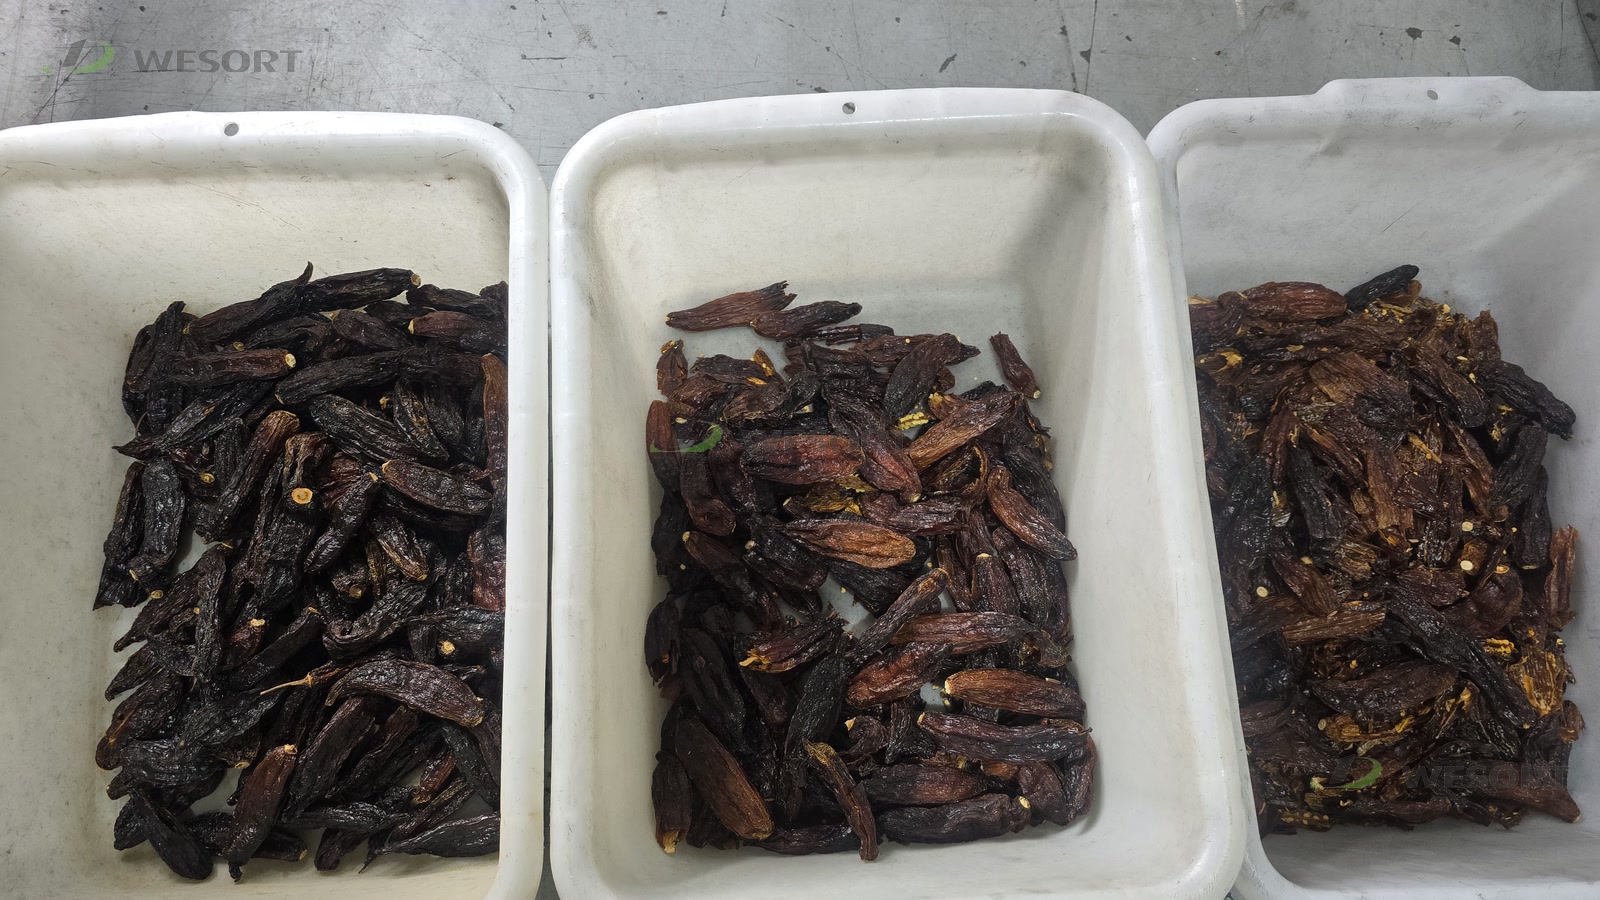
A mixed lot of dried chili rarely has just one problem. Dark pods sit beside red-brown pods, whole product is mixed with broken pieces, and stems or fibrous material remain in the flow. WESORT helps processors turn that mixed lot into clearly defin...
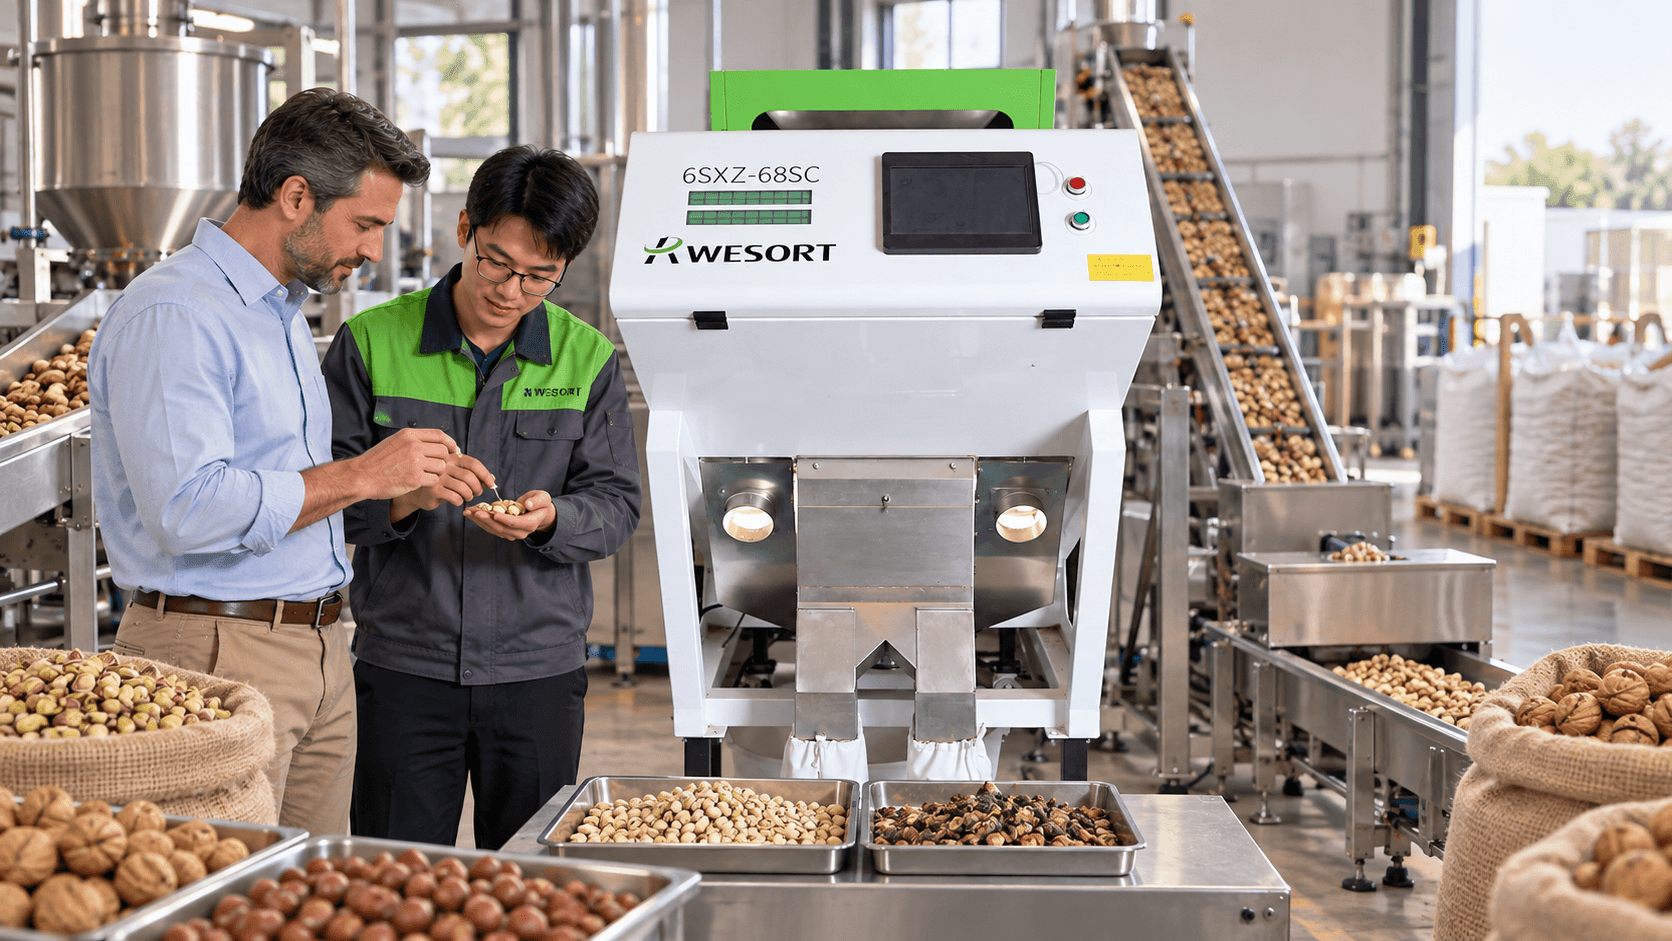
A reliable nut color sorter manufacturer should be able to prove three things before asking you to buy: that your actual material can be separated, that the proposed machine fits your production line, and that technical support will still be availa...
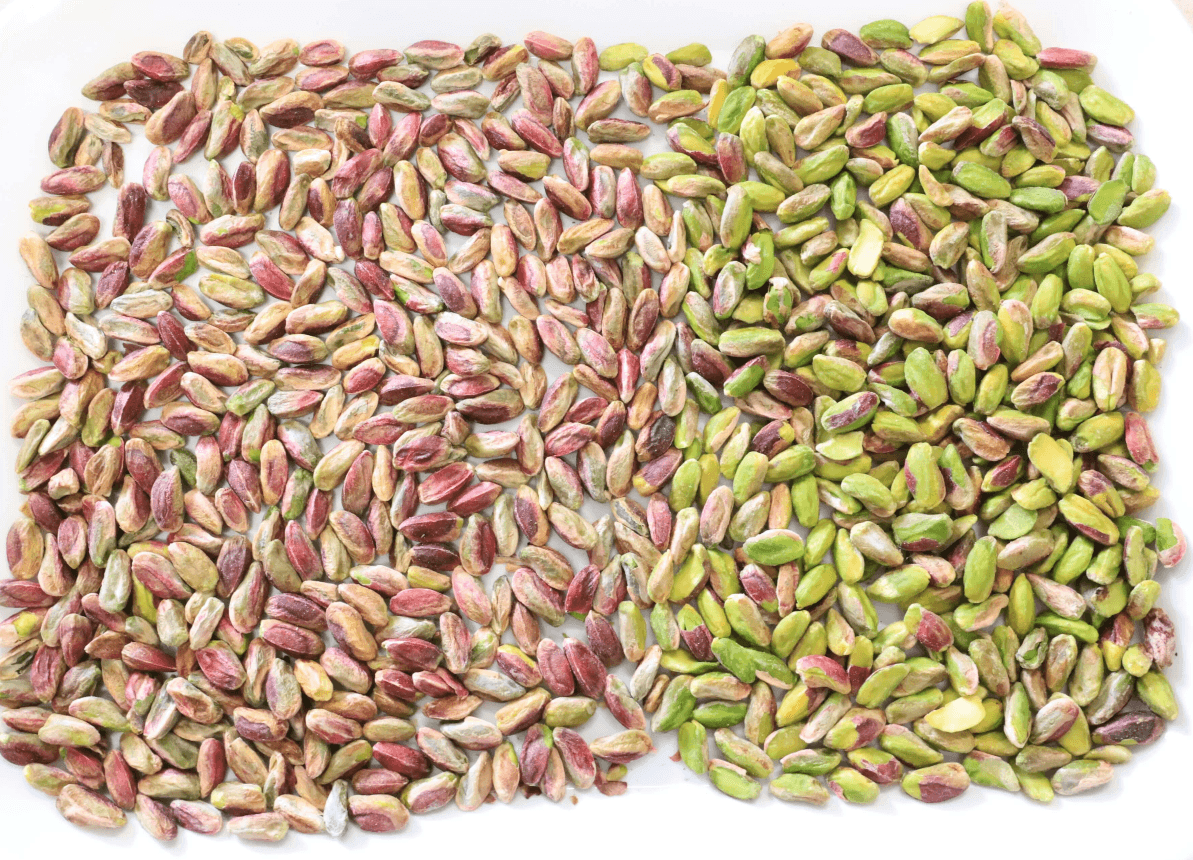
A pistachio sorter should be configured for the material entering it, not for the word “pistachio” alone. An in-shell line may need to separate open and closed shells. A kernel line may need color grades and removal of broken or dark pieces. A post...
Choosing the right pistachio sorting machine in Turkey is not simply a matter of comparing machine width, number of chutes or advertised capacity. For pistachio processors, the more important question is: What exactly does the machine need to sep...
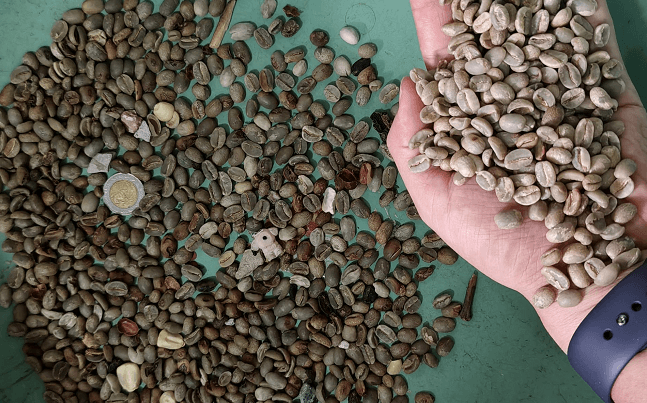
Choosing a coffee sorting machine in Colombia should not begin with the number of chutes or a headline capacity. It should begin with five facts about the coffee entering your line and the product you need to deliver. Without them, two machines th...
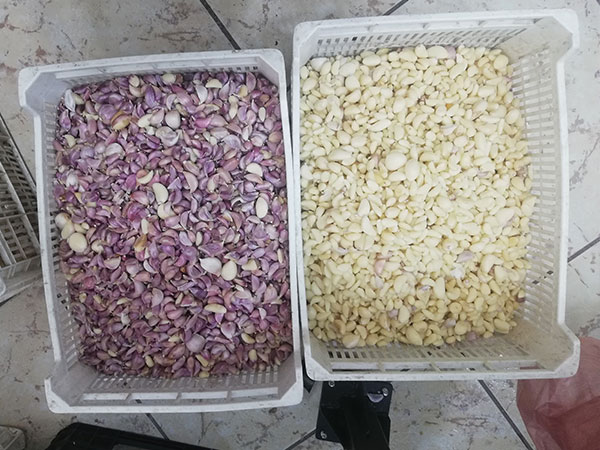
A garlic sorting machine can separate cloves that differ visibly from the accepted product in color, skin coverage, shape, size or surface condition. Typical targets include cloves with attached purple skin, incomplete peeling, yellow or brown disc...
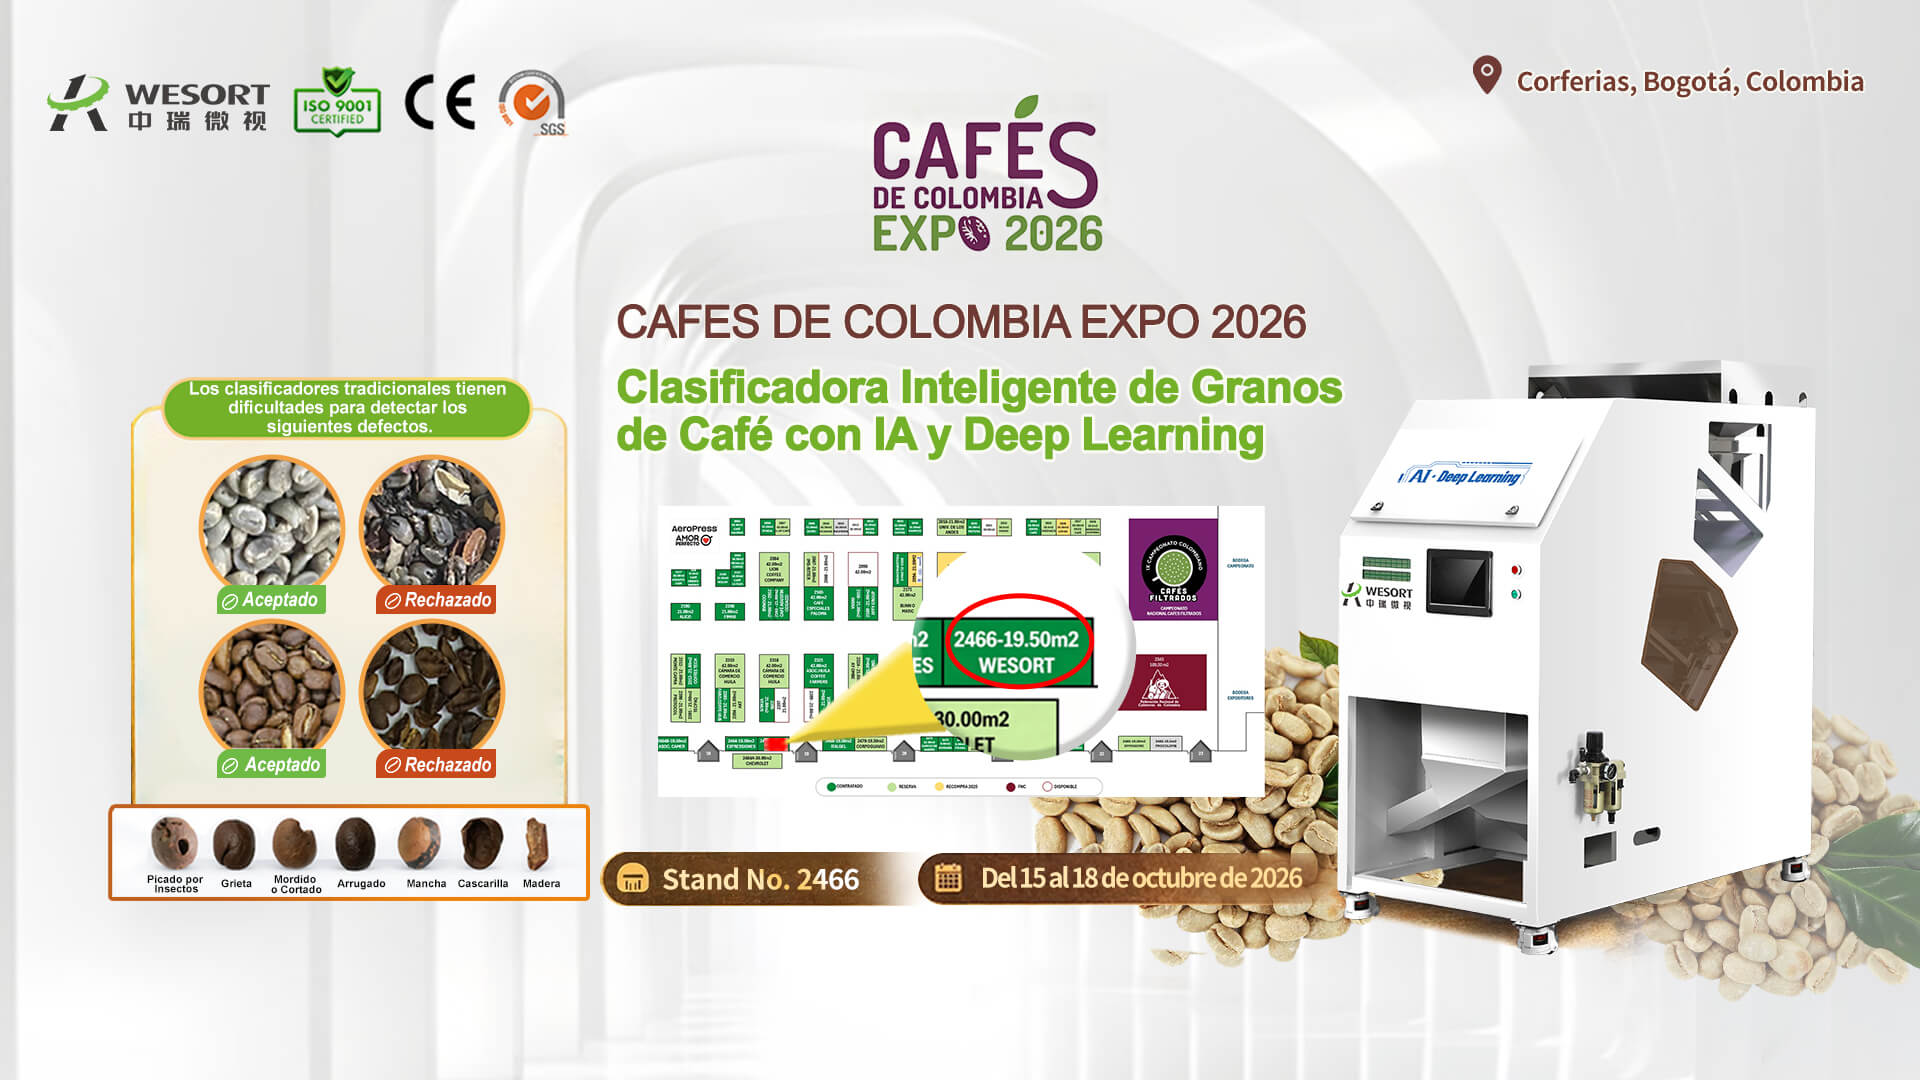
Don’t bring only a business card. Bring the coffee your team is struggling to sort. From October 15 to 18, WESORT will be at Cafés de Colombia Expo 2026 in Bogotá. At Booth 2466, visitors can see how optical sorting responds to real coffee material...
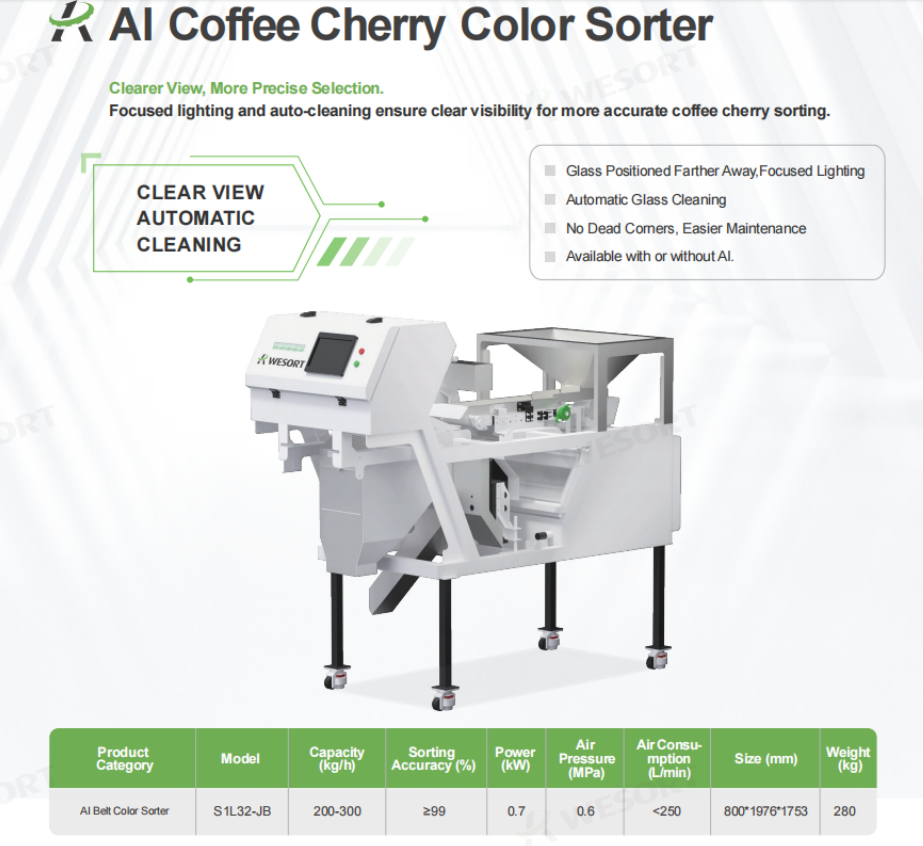
Industry Background and Problem Introduction Coffee processing combines natural variation in agricultural material with increasingly specific buyer and quality requirements. Fresh coffee cherries, parchment coffee, green beans and roasted beans are d...
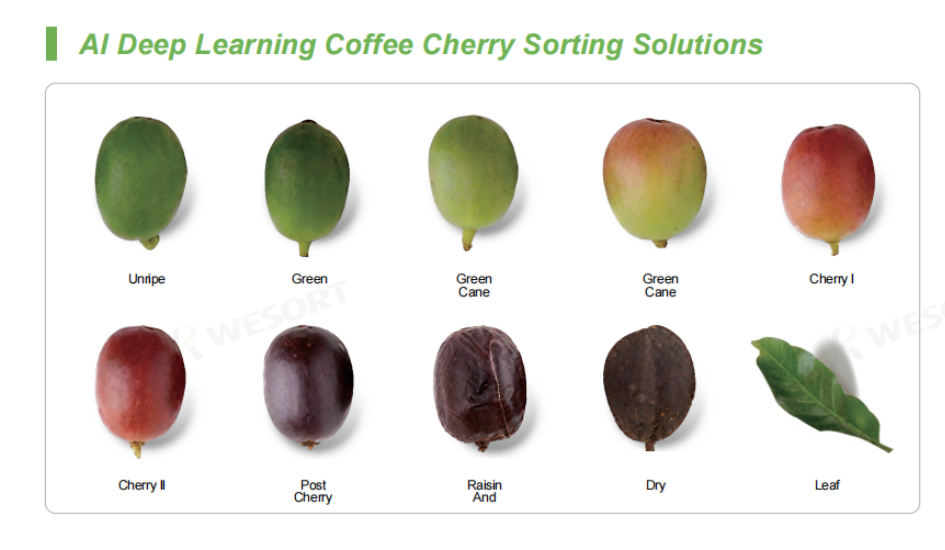
Sorting fresh coffee cherries before pulping or drying can help a processor separate visibly different fruit into more consistent lots. The right approach depends on the cherries, the acceptance standard and where the sorter will sit in the processin...
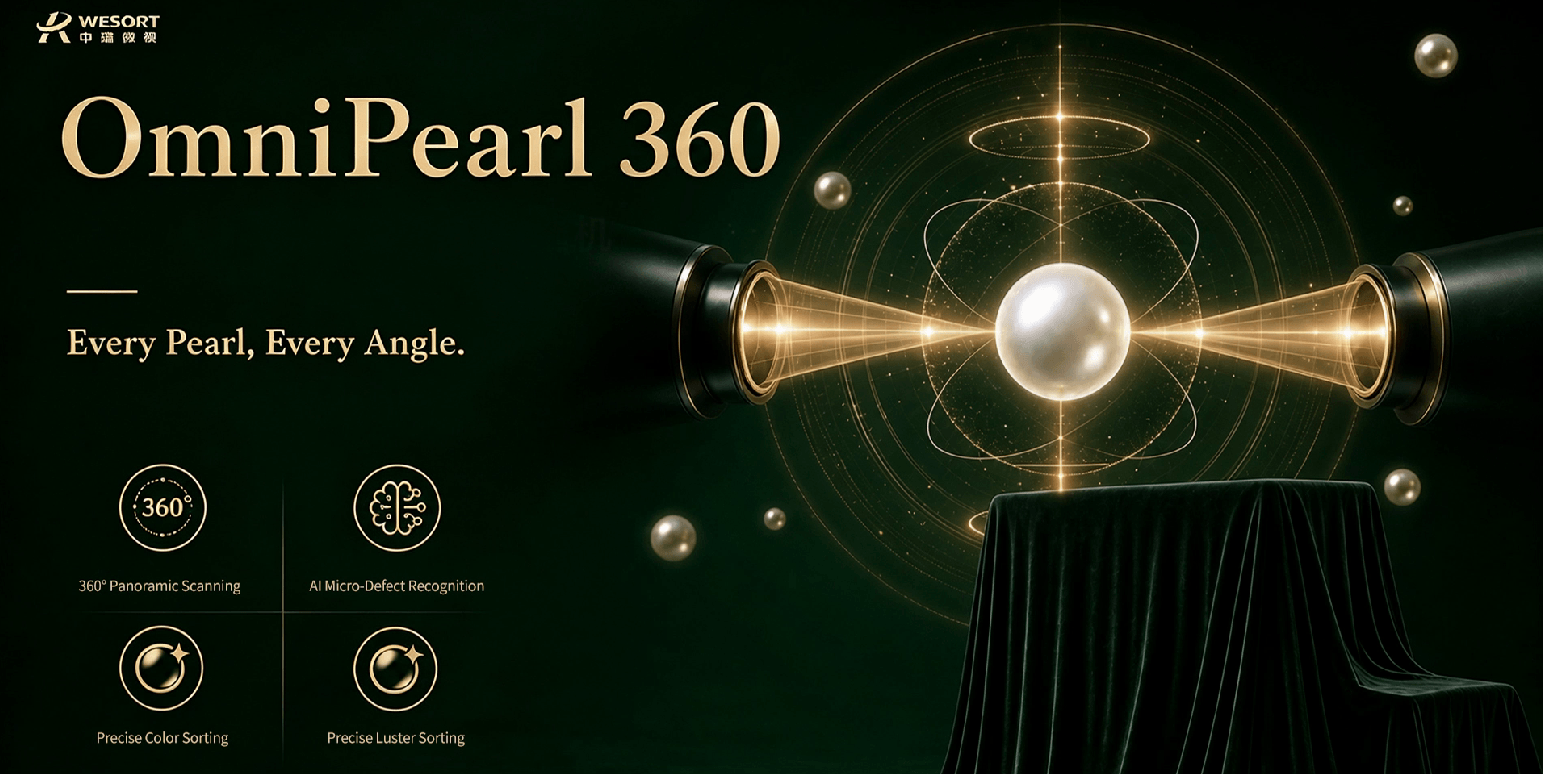
Every Pearl, Every Angle. 360° PANORAMIC AI PEARL SORTING The hardest part of pearl sorting is not seeing a pearl once. It is seeing enough of its surface to make a consistent decision. A dark spot may sit on the back. A fine crack may become visible...
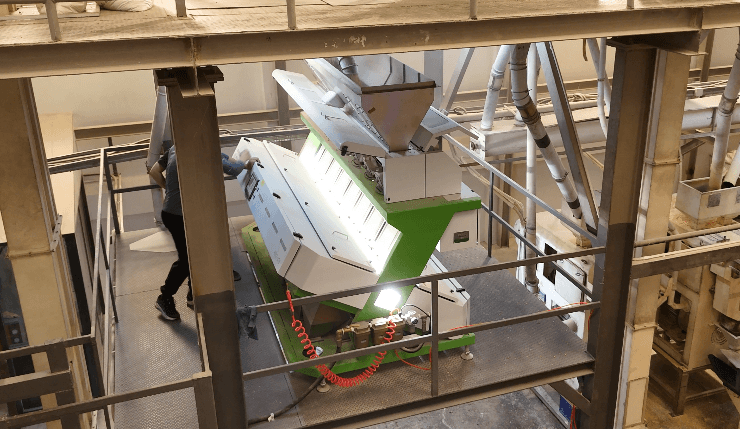
A practical way to choose a corn sorting machine is to compare your plant with corn processors that have already solved similar problems. WESORT has supplied corn sorting solutions for different production scales, from a dual-channel white-corn pro...
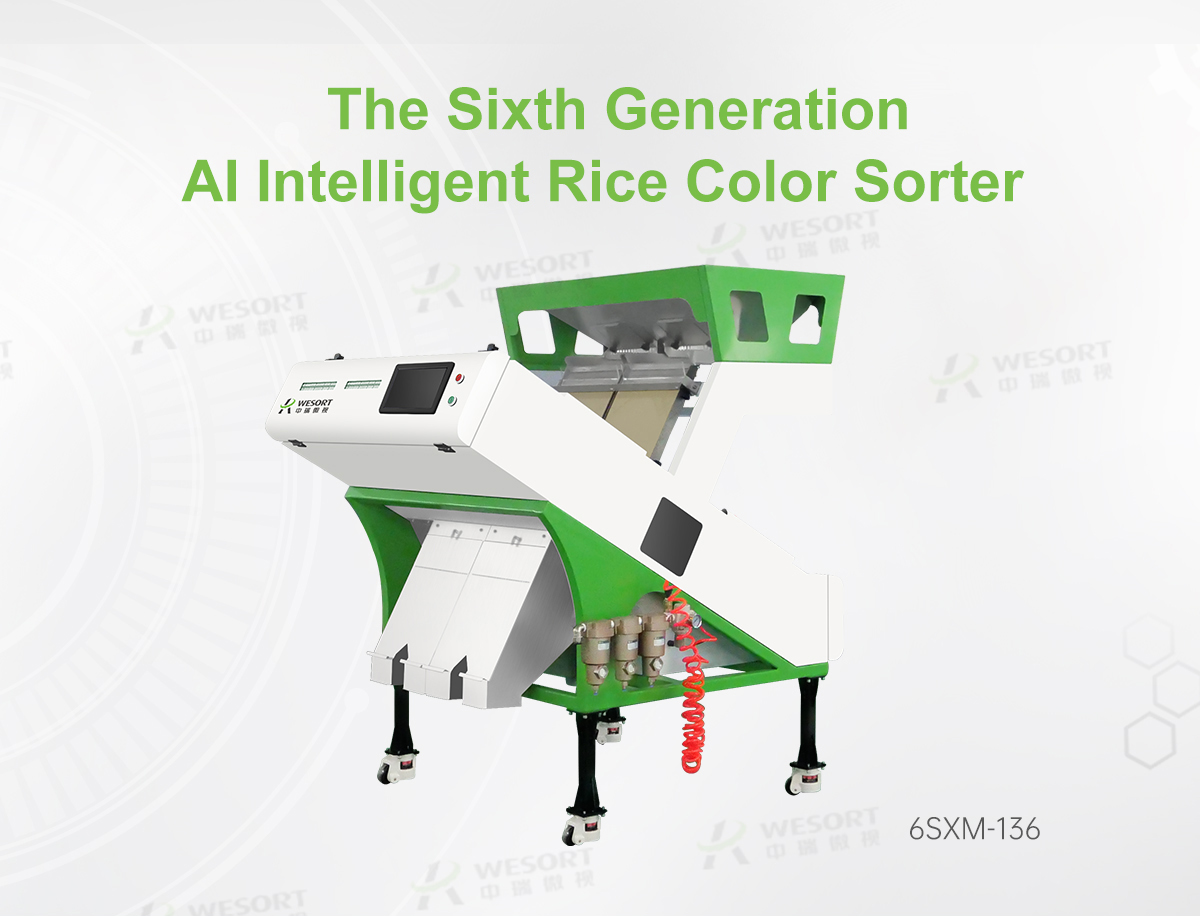
An optical rice sorter improves purity by turning visible differences into controlled separation decisions. Stable feeding presents the rice, illumination and cameras capture visible characteristics, software evaluates color and shape, and precisio...
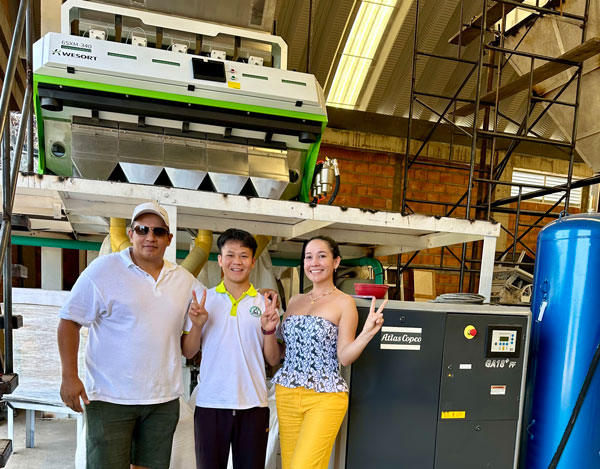
Choose a rice sorting machine by matching the rice variety, target defects, required throughput, finished-product standard, acceptable loss of good rice, and site utilities. Compare machines only after testing representative material and reviewing bo...
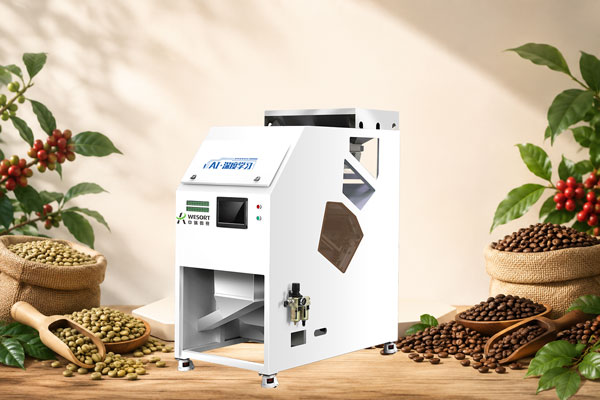
Coffee processors face a constant challenge when it comes to maintaining consistent quality across green and roasted coffee beans. Quakers, scorched beans, abnormal-color beans, broken beans, and foreign materials can affect the appearance and consis...
Mexico has a strong coffee-processing industry, with coffee producers and processors facing increasingly demanding requirements for quality, consistency, and production efficiency. From coffee cherries and green coffee beans to roasted coffee, effect...
Coffee quality control depends heavily on the equipment used to remove defective beans, foreign materials, and quality inconsistencies before roasting or export. For coffee processors, roasteries, and exporters, AI-powered optical color sorters h...
Coffee processors around the world are under growing pressure to deliver consistent quality while controlling costs and meeting strict export standards. Manual sorting—long the default method for removing quakers, scorched beans, and foreign matter...
Upgrade Your Sorting Solution with Exclusive Benefits In 2026. WESORT continues to move forward with innovation, quality, and commitment. We sincerely appreciate the trust and support from customers around the world. To give back to our global ...
The best bean-sorting result does not begin with a machine setting. It begins with a clear description of the beans you want to pack, the defects your buyer rejects and the amount of good product you are prepared to lose. Short answer: clean and s...
When nut processing enters its busiest weeks, inconsistent raw material, visible defects and foreign materials can quickly become production problems. For processors handling hazelnuts, pistachios, almonds, pecans, Brazil nuts, peanuts and other nut...
A mixed lot of dried chili rarely has just one problem. Dark pods sit beside red-brown pods, whole product is mixed with broken pieces, and stems or fibrous material remain in the flow. WESORT helps processors turn that mixed lot into clearly defin...
A reliable nut color sorter manufacturer should be able to prove three things before asking you to buy: that your actual material can be separated, that the proposed machine fits your production line, and that technical support will still be availa...